



Injection Mold Components: Main Parts and What Each One Does
Injection mold components include the core, 空洞, runner system, 冷却チャネル, 排出システム, guide pillars, and support plates. Each part controls a different stage of the molding cycle, from shaping and cooling to alignment and ejection. Understanding how these systems work together helps manufacturers reduce defects, improve cycle time, and choose the right mold design for production needs.
Injection molds look simple from the outside, but inside they contain multiple precision systems working together under high pressure and temperature. A small issue in cooling, アライメント, or ejection can affect part quality, サイクルタイム, そしてカビの寿命. このガイドでは、主な金型の構成要素について説明します, what each one does, and how they influence real production performance.
What are the main injection mold components?
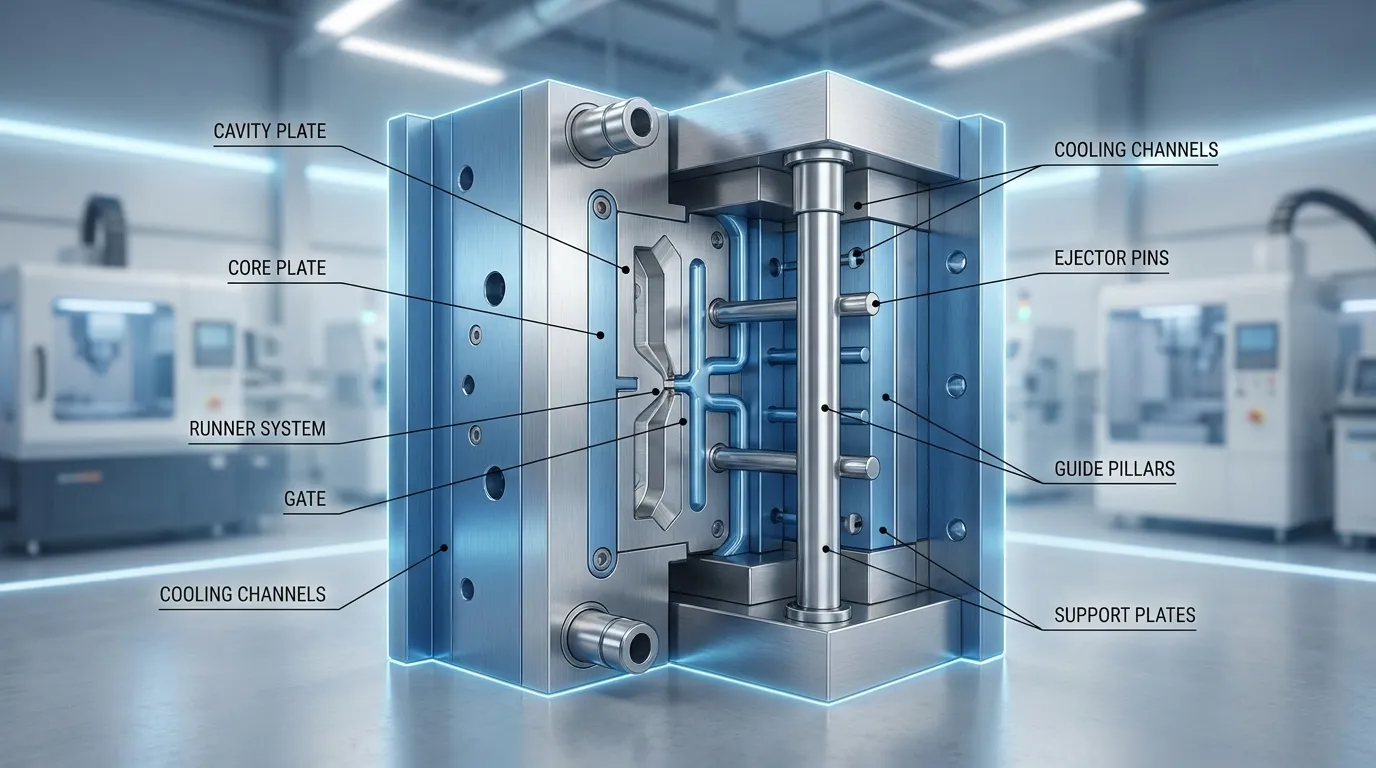
Injection mold components work together to guide molten plastic, shape the part, cool it evenly, and eject it safely after solidification. The main systems include the core and cavity, ランナーとゲートシステム, 冷却チャネル, 排出システム, guiding components, and mold base structure.
An injection mold is built from several connected systems instead of a single block of steel. Each system handles a specific function during the molding cycle. Some parts shape the plastic, others manage heat, and others control movement and alignment.
The mold base supports the entire structure and holds the internal components in position. Inside the mold, molten plastic enters through the feed system, fills the cavity, cools down, and is ejected after solidification. それによると 射出成形プロセスの概要, molds typically contain separate injection and ejection sides that open and close during production.
| コンポーネントシステム | 主な機能 | 共通生産リスク |
|---|---|---|
| コアとキャビティ | プラスチック部分の形状を作ってください | 次元誤差 |
| ランナーとゲートシステム | ガイドの溶融プラスチック | ショートショットやバランスの崩れ |
| 冷却チャネル | 熱を取り除く | ワーページ |
| 排莢システム | 完成した部分を取り除いてください | 表面の痕跡 |
| ガイドピラーとブッシング | アライメントを維持 | フラッシュ |
| 支持板 | 圧力負荷の取り扱い | 型の摩耗 |
If you want a broader overview of how molds operate inside the full production cycle, これだ プラスチック射出成形プロセス guide explains the complete workflow.
コアとキャビティの違いは何ですか??
空洞はプラスチック部品の外形を形成します, while the core creates the internal geometry. Together, these two mold halves define the final dimensions, 壁の厚さ, and surface quality of the molded component.
The cavity side usually stays on the fixed half of the mold. It shapes the outer surface that customers see after molding. Surface texture, 外観仕上げ, and visible details often come from the cavity surface.
The core side usually sits on the moving half of the mold. It creates internal features such as holes, リブ, スロット, and hollow sections. During ejection, the molded part normally stays attached to the core side because shrinkage tightens around the core.
| 特徴 | キャビティ | コア |
|---|---|---|
| 主な役割 | 表面外の形態 | 内部幾何学 |
| 型の位置 | 固定側 | 移動面 |
| 表面フォーカス | 外観仕上げ | 構造の詳細 |
| 射出側 | 通常はリリースする部分 | 通常は関与しています |
Poor machining or wear in either section can create dimensional variation. Even slight misalignment between the core and cavity may cause flash around the parting line. This becomes more critical in tight-tolerance applications such as medical housings or precision electronics.
For a deeper look at overall mold architecture, see these 型構造の基本.
How does the feed system move plastic through the mold?
The feed system guides molten plastic from the injection machine into the mold cavity. It includes the sprue bushing, ランナー, and gates, all of which control pressure, material distribution, and filling consistency.
The feed system acts like a controlled pathway for molten resin. Plastic first enters through the sprue bushing, then travels through runners before passing into the cavity through the gate. Every section affects filling speed, 圧力, and balance.
What does a sprue bushing do?
The sprue bushing connects the molding machine nozzle to the mold. It handles the first stage of material transfer and directs molten plastic into the runner system. Poor sprue design can create leakage, pressure loss, or uneven filling.
なぜマルチキャビティ型でランナーバランスが重要なのか
Runner layout becomes more important in multi-cavity molds because every cavity must fill evenly. If one runner path is longer than another, cavities may fill at different speeds. This can create dimensional variation between parts.
A packaging mold with uneven runner lengths may produce one cavity with excess flash while another shows short shots. Balanced runner systems reduce this risk and improve production consistency.
The gate controls how molten plastic enters the cavity. Smaller gates reduce visible marks, but they can restrict flow in thicker parts. Larger gates improve filling but may increase trimming work after molding.
More cooling channels do not automatically improve molding quality. Poorly balanced cooling and feed layouts can still create uneven shrinkage and warpage even when flow rates appear acceptable.
For a broader explanation of filling and molding stages, これだ 射出成形のワークフロー covers the full production sequence.
Why is the cooling system critical in injection molding?
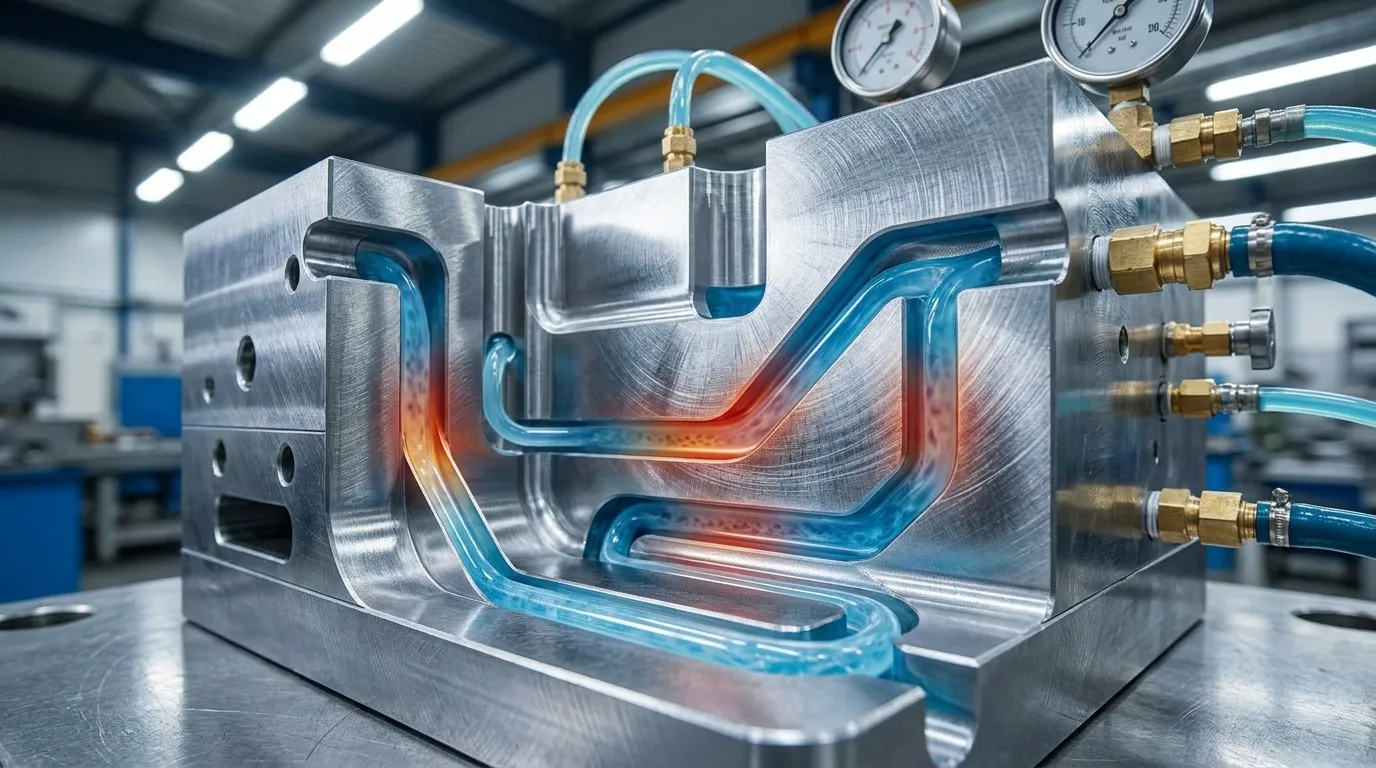
Cooling channels remove heat from the mold after plastic fills the cavity. Proper cooling improves cycle time, 次元安定性, and surface quality while reducing warpage and uneven shrinkage.
Cooling often controls most of the molding cycle time. If heat stays trapped inside the mold too long, production slows down and part dimensions become less stable. 次の通りです RapidDirectの金型部品ガイド, cooling systems also help reduce mold wear by controlling thermal stress.
Cooling channels are drilled through the mold base around the cavity and core. Water or coolant circulates through these channels to remove heat evenly. Placement matters because uneven cooling creates uneven shrinkage.
A medical housing mold may develop warpage if cooling channels sit too far from one side of the cavity. One side cools faster while the opposite side continues shrinking, causing the finished part to twist slightly after ejection.
| もしこれが起きたら | 冷却問題 | 典型的な結果 |
|---|---|---|
| あるエリアは冷えが遅いです | チャンネル配置の不備 | ワーページ |
| 冷却は不均一です | 温度の不均衡 | 収縮変動 |
| カビは高温のままです | ゆっくりとした熱除去 | サイクル時間の延長 |
| ホットスポットの形成 | 冷却材流量が限られている | 表面欠陥 |
More cooling channels are not always better. Excessive channel density can weaken steel sections or create uneven thermal behavior. 多くの場合, balanced cooling design matters more than maximum cooling volume.
Applications with tight tolerances often require advanced thermal control. これらは 精密成形の応用 show where cooling consistency becomes critical.
What does the ejection system do?
The ejection system removes the molded part from the core side after cooling. Ejector pins are the most common method, but sleeves and stripper plates may be used for delicate or deep components.
型が開いた後, the molded part usually remains attached to the core side. The ejection system pushes the part free without damaging surfaces or deforming thin sections.
Ejector pins are the most widely used method because they are simple and cost-effective. Pins push directly against selected points on the part surface. 配置の悪さ, しかし, can leave visible pin marks or create stress points.
A high-volume packaging mold may show ejector pin wear after extended production cycles. 時間をかけて, repeated movement creates friction and surface wear that transfers onto cosmetic areas of the molded part.
- イジェクターピン
- イジェクタースリーブ
- ストリッパープレート
- リターンピン
- エジェクタープレート
Slides are not always the best solution for difficult ejection. Straight-pull designs are often easier to maintain and reduce downtime risk when geometry allows simpler mold movement.
For additional details on ejector hardware and layout, これらは エジェクターシステム構成要素 explain the full structure.
How do guide pillars and support plates keep molds aligned?
Guide pillars and bushings keep the mold halves aligned during every production cycle. Proper alignment prevents flash, 不均一な摩耗, 次元変動, and premature mold damage.
Guide pillars and bushings control mold alignment during opening and closing. These components ensure the core and cavity meet in the correct position under clamping pressure. Even small alignment errors can affect part quality.
A consumer electronics mold may begin producing flash after guide bushings wear down. The mold halves no longer close perfectly, allowing molten plastic to escape along the parting line.
Support plates handle the heavy mechanical loads generated during injection. Without adequate support, mold plates may flex under pressure, especially in large or multi-cavity molds.
- ガイドピラー
- ガイドブッシング
- 支持板
- クランププレート
- スペーサーブロック
次の通りです FirstMoldの射出成形ガイド, guiding structures play a major role in maintaining molding accuracy and protecting mold life.
For a closer look at structural mold systems, これらをレビューしてください 型台システム.
What are slides and lifters used for in complex molds?
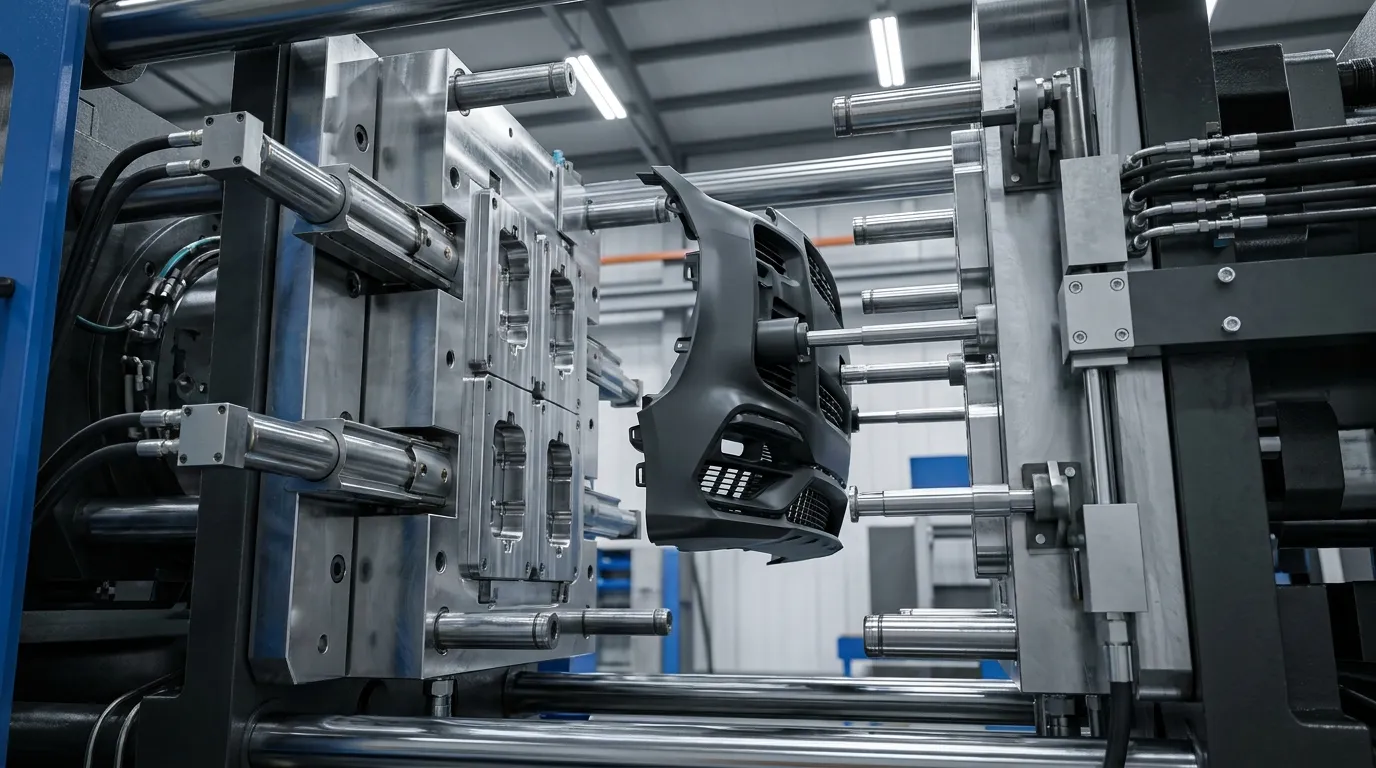
Slides and lifters allow molds to release parts with undercuts or side features that cannot eject straight out of the cavity. These moving components increase mold complexity but are essential for many functional plastic parts.
Some plastic parts contain side holes, clips, hooks, or undercuts that prevent straight ejection. Slides and lifters solve this problem by moving sideways or at an angle during mold opening.
カビにサイドアクションが必要な場合
An automotive clip with locking tabs may require side actions because the undercut geometry traps the part inside the mold. Without slides, the part could not eject without damage.
Slides move perpendicular to the mold opening direction, while lifters move upward at an angle during ejection. それによると 射出成形の参考文献, these systems are commonly used for undercut release in complex parts.
These systems increase tooling cost because they require additional machining, wear surfaces, and moving assemblies. They also add maintenance requirements during long production runs.
Multi-cavity molds are not always the best option when slides are involved. Complex side actions increase alignment sensitivity and raise downtime risk if maintenance intervals are ignored.
これらの特徴の例は以下で見ることができます 複雑な成形部品 used across automotive and industrial products.
Which injection mold components affect part quality the most?
Part quality depends heavily on cooling balance, venting efficiency, アライメント精度, and controlled ejection. Even small design errors in these systems can create flash, 陥没痕, 焼け跡, or dimensional instability.
Several mold systems directly influence cosmetic quality and dimensional accuracy. Problems often appear when one system works correctly while another becomes unstable.
Poor venting is a common example. Trapped air inside the cavity can create burn marks or incomplete filling. 次の通りです エラストロンの成形欠陥ガイド, weak venting is one of the major causes of gas-related molding defects.
| 欠陥 | 関連コンポーネント | 原因としては | 共通訂正 |
|---|---|---|---|
| フラッシュ | ガイドシステム | ミスアライメント | 摩耗したブッシュの交換 |
| ワーページ | 冷却システム | 不均一な冷却 | リバランスチャネル |
| 焼け跡 | 換気システム | トラップガス | 換気の改善 |
| ピンマーク | 排莢システム | ピンの配置が悪い | エジェクターの配置を調整する |
| 次元変動 | ランナーシステム | アンバランス・フィリング | 正しいランナーの長さ |
A multi-cavity mold with uneven runners may fill some cavities faster than others. One part may shrink differently even when machine settings stay unchanged. Balanced flow design reduces this variation.
Cooling balance matters more than cooling quantity. Adding more channels without proper placement can create temperature differences that increase warpage instead of reducing it.
For a broader explanation of molding consistency and defect prevention, これだ 成形品質係数 guide covers the full production picture.
How do mold components influence tooling cost and maintenance?
Complex mold components increase tooling cost because they require tighter machining tolerances, additional assemblies, and more maintenance planning. Cooling layouts, スライド, multi-cavity systems, and wear surfaces all affect long-term production cost.
Simple two-plate molds are easier to machine and maintain. Once slides, リフター, and advanced cooling systems are added, manufacturing complexity rises quickly. More moving parts also increase inspection and replacement requirements during production.
| コンポーネント特徴 | コスト影響 | メンテナンスへの影響 |
|---|---|---|
| マルチキャビティレイアウト | 加工精度の向上 | さらなるバランスチェック |
| スライドとリフター | 追加の移動集会 | 摩耗リスクの高さ |
| 高度な冷却 | 複雑な掘削とルーティング | 掃除の必要性が増えました |
| ホットランナーシステム | 初期金型コストの高さ | 電気保守 |
Wear components usually require the most attention. 門, イジェクターピン, ガイドブッシング, and moving slide surfaces experience repeated friction during production cycles.
A simpler mold is sometimes the safer long-term choice. Lower-volume projects may not benefit from highly complex tooling if maintenance downtime offsets production speed gains.
次の通りです EWMFGの金型成分ガイド, mold structure and system complexity directly affect durability and operational efficiency.
次のステップを正しく進める
Understanding injection mold components helps buyers and engineers make better tooling decisions before production begins. Small details such as cooling layout, runner balance, or guide wear can affect cycle time, 部品品質, and maintenance cost far more than many first-time buyers expect.
If you're evaluating a new mold design, focus on how the systems work together instead of looking at components individually. A balanced mold usually performs better, lasts longer, and creates fewer production problems over time. For a broader view of tooling strategy and mold engineering, reviewing a complete molding guide can help connect these systems to the full manufacturing process.
よくある質問
What are the main components of an injection mold?
The main injection mold components include the core, 空洞, sprue bushing, runner system, 門, 冷却チャネル, 排出システム, guide pillars, and support plates. Each system controls a different stage of the molding cycle, from filling and cooling to alignment and part removal.
What does an ejector pin do in injection molding?
An ejector pin pushes the cooled plastic part off the core side after molding is complete. Poor ejector pin placement can leave visible marks or damage delicate surfaces during removal.
なぜ射出成形で冷却チャネルが重要なのか?
Cooling channels remove heat from the mold to control cycle time and part stability. Uneven cooling can cause warpage, shrinkage differences, and inconsistent dimensions across molded parts.
コアとキャビティの違いは何ですか??
The cavity forms the outside shape of the plastic part, while the core forms the internal geometry. These two mold surfaces close together to create the final molded structure.
What causes flash in injection molding?
Flash usually happens when mold halves do not align correctly or when pressure escapes at the parting line. Worn guide components and poor clamping conditions are common causes of this defect.
What are slides and lifters used for?
Slides and lifters help release parts with undercuts or side features that cannot eject straight out of the mold. They allow more complex geometries but increase tooling complexity and maintenance needs.
どの金型部品が最も早く摩耗しますか?
門, イジェクターピン, スライド, ガイドブッシング, and high-friction surfaces usually wear faster than structural plates. Wear rates increase in high-volume production and abrasive material applications.



サンシャインより書かれました
サンシャインで, 私たちは精密金型部品の専門製造およびサプライヤーです, プレスおよび射出成形用途向けの幅広い製品を提供しています. 私たちの主な焦点はパンチダイスです, イジェクターピンとスリーブ, ガイドポストとブッシング. 高度なCNC加工技術で, 厳格な品質管理, そして強力な生産能力, 私たちは信頼性を保証しています, 高精度部品, また、迅速かつ効率的なグローバル供給のための在庫の標準部品も併用しています.
ニュース
サービスを受けましょう
あらゆる予算に合った高品質な部品と、親切なスタッフが訓練されていて、訪問を有益で手間なく充実させてくれます.
