



入荷および通常の品質管理のためのパンチピン検査チェックリスト
A punch pin inspection checklist should answer four questions: Is this the correct punch? Does it match the approved specification? Is it still fit for service? What action should follow the inspection?
This guide covers individual punch pins used in metal-stamping dies. Incoming QC verifies a newly supplied punch against the purchase order, 図面, revision, および必要な書類. Routine QC checks whether a punch remains serviceable after production use, regrinding, a collision, or another abnormal event.
Punch pins work within a larger die system. Guides, ブッシング, retainers, stripper components, die clearance, and alignment can all influence punch condition. The broader roles of these components are covered in the ダイ部品ガイド (推論). はい, the focus stays on inspecting and dispositioning the punch pin itself.
No universal tolerance, inspection interval, or wear limit applies to every punch pin. Acceptance must be based on the approved drawing, purchase specification, control plan, or another documented requirement.
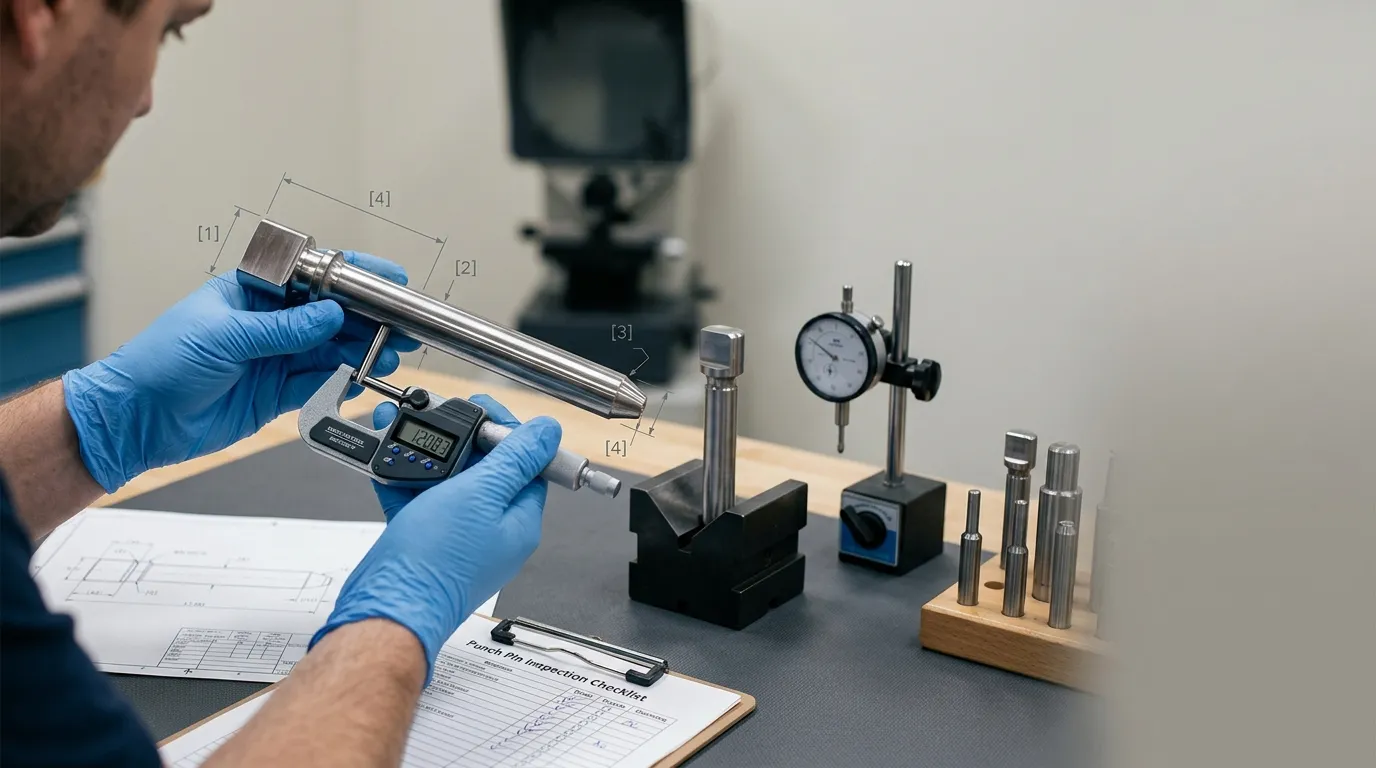
入ってくるQCと通常のQCは異なるリスクを取る
Incoming and routine inspection use many of the same instruments, but they answer different questions.
| 検査段階 | 主な目的 | 典型的なチェック | 主な決定 |
|---|---|---|---|
| QCが入ってくる | 供給されたパンチが注文および承認された仕様に一致しているか確認してください | Part identity, 図面の改訂, material or coating documents, visible damage, 寸法, 幾何学, inspection report | Accept, hold, return, or reject |
| ルーチンQC | 使用済みのパンチが安全かつ機能しているか確認してください | エッジの摩耗, ひび割れ, 腹立たしい, 次元変化, ランアウト, 作業長, 生産症状, regrind history | 復帰, モニター, regrind, 置き換え, or investigate |
| 再研磨後の検査 | 研ぎ直しで他の特徴が受け入れられないことなくエッジが元に戻ったか確認してください | Edge form, burr removal, 全長, 作業長, プロフィール, 表面状態 | Release, リワーク, または置き換え |
| イベント後の検査 | Check for hidden or visible damage after a jam, collision, misfeed, or nearby breakage | ひび割れ, 曲げる, head damage, ランアウト, 座席面, 結合成分 | Quarantine, 調査, 修理, または置き換え |
Incoming inspection should establish a reliable baseline. Recording the punch’s as-received dimensions and condition makes later wear easier to identify.
Routine inspection compares the current punch against that baseline and any approved service limits. A punch can remain within its original manufacturing tolerance yet show an abnormal wear trend. 逆に, a worn feature may still appear visually acceptable while no longer meeting the documented service requirement.
Prepare the Punch, 文書, and Measuring Equipment
Inspection should not begin with a caliper. It should begin with the correct documents, part identity, and measurement conditions.
- Confirm the inspection stage. Record whether the punch is incoming, in routine service, newly reground, or being checked after an abnormal event.
- Obtain the approved drawing. Verify the drawing number and revision before measuring anything. An accurate measurement against an obsolete revision is still an invalid inspection result.
- Review the purchase and quality requirements. Check the purchase order, control plan, approved sample, inspection-report requirement, and any requested material, 熱処理, 硬度, またはコーティングの文書.
- Match the punch to its records. Confirm the part number, lot or serial number, quantity, material designation, coating designation, and any engraved identification.
- Inspect the packaging before cleaning. Record impact damage, 腐食, broken protective packaging, loose punches, or signs that sharp edges contacted each other during transport.
- Clean the punch carefully. Remove oil, dirt, チップス, and transferred material without rounding the cutting edge or scratching a coated surface. Residue on a diameter or seating face can affect the measurement.
- Stabilize the part when tolerances are tight. A punch arriving from a hot production area, cold warehouse, or vehicle may need time to reach the inspection environment. Temperature differences can affect dimensional results.
- Verify the measuring equipment. Check instrument identification, calibration status, measuring range, 解決, 接触条件, and cleanliness. Confirm that any V-block, center, 試合, or surface plate is also clean and suitable for the feature.
SunshinePro states that non-standard mold parts can be processed from customer drawings, while its punch-pin page lists diameter, 長さ, 頭部スタイル, マテリアルグレード, and coating as customizable characteristics. Those fields should therefore be treated as drawing- and order-specific requirements rather than assumed product defaults.
測定前に矛盾または欠落している仕様を解決する
Do not select a tolerance from memory, an old inspection sheet, or a generic catalog.
Place the punch on hold when:
- the drawing revision does not match the purchase order;
- the inspection report refers to another part or lot;
- the drawing and purchase specification contain conflicting limits;
- the material or coating designation is missing;
- the required datum or measurement method is unclear;
- an approved deviation is mentioned but not supplied.
Obtain written clarification from the responsible engineer, customer, or supplier before assigning a pass or fail result. The controlling-document hierarchy should follow the customer’s quality system or contract rather than an informal assumption.
すべてのパンチ機能に目に見えるダメージがないか確認してください
Visual inspection is the fastest way to find obvious defects, but it should follow a consistent feature-by-feature sequence.
Use clean lighting and suitable magnification. Rotate the punch and inspect the complete circumference rather than viewing only one side.
| 検査区域 | 確認すべき条件 | 可能な意義 | 典型的な次の行動 |
| カッティングエッジと先端 | チップ, ひび割れ, エッジの丸みを一つ, バー, 変形, ピックアップ | Loss of cutting quality, local overload, 影響, 使用期間, adhesive material transfer | 測定, quarantine, regrind, または置き換え |
| シャンクまたはボディ | 得点, 腹立たしい, wear bands, 腐食, 悩む, 資料の転送 | Poor guidance, 摩擦, ミスアライメント, lubrication problem, 誤ったフィット | きれいだ, measure diameter/runout, inspect mating parts |
| ヘッド&ショルダー | Mushrooming, ピーニング, ひび割れ, uneven seating marks, 変形 | 過負荷, incorrect seating, retainer problem, 不十分な支援 | 隔離とリテーナーや座席状況の検査 |
| 遷移半径 | ひび割れ, grinding marks, abrupt surface changes | 応力集中, grinding damage, fatigue initiation | Magnify, escalate, または置き換え |
| コーティングされた表面 | Peeling, 剥がれ, 引っかき傷, 変色, 露出基質 | Coating damage, 摩擦, 影響, 腐食, 使用期間 | Record location, assess function, seek engineering review |
| 識別マーク | Missing or illegible part, lot, or serial information | トレーサビリティの喪失や改訂の混合リスク | 身元が確認されるまで待機してください |
A small chip at the cutting edge is not equivalent to a superficial scratch on a non-working surface. The inspection record should state the defect location, approximate extent, and whether it affects a functional feature.
ひび割れ, 重度の変形, or a damaged retention head generally justify immediate quarantine. 苛立たしい, ピックアップ, or one-sided scoring may require inspection of the die system as well as the punch. Detailed causes of cracking and catastrophic failure belong in the guide to プレス金型のパンチ破損.
目視検査では確認できないこと
Visual inspection cannot reliably establish:
- exact body or tip diameter;
- overall or working length;
- 直線性;
- ランアウト, 同心円, or coaxiality;
- shaped-tip profile;
- numerical surface roughness;
- マテリアルグレード;
- heat-treatment conformity;
- 硬度;
- coating identity.
A punch may look undamaged but still be dimensionally out of tolerance. 材料等級, 硬度, and coating conformity may require traceable documentation or a specified test method.
フィット感や機能を制御する寸法と幾何学を測定してください
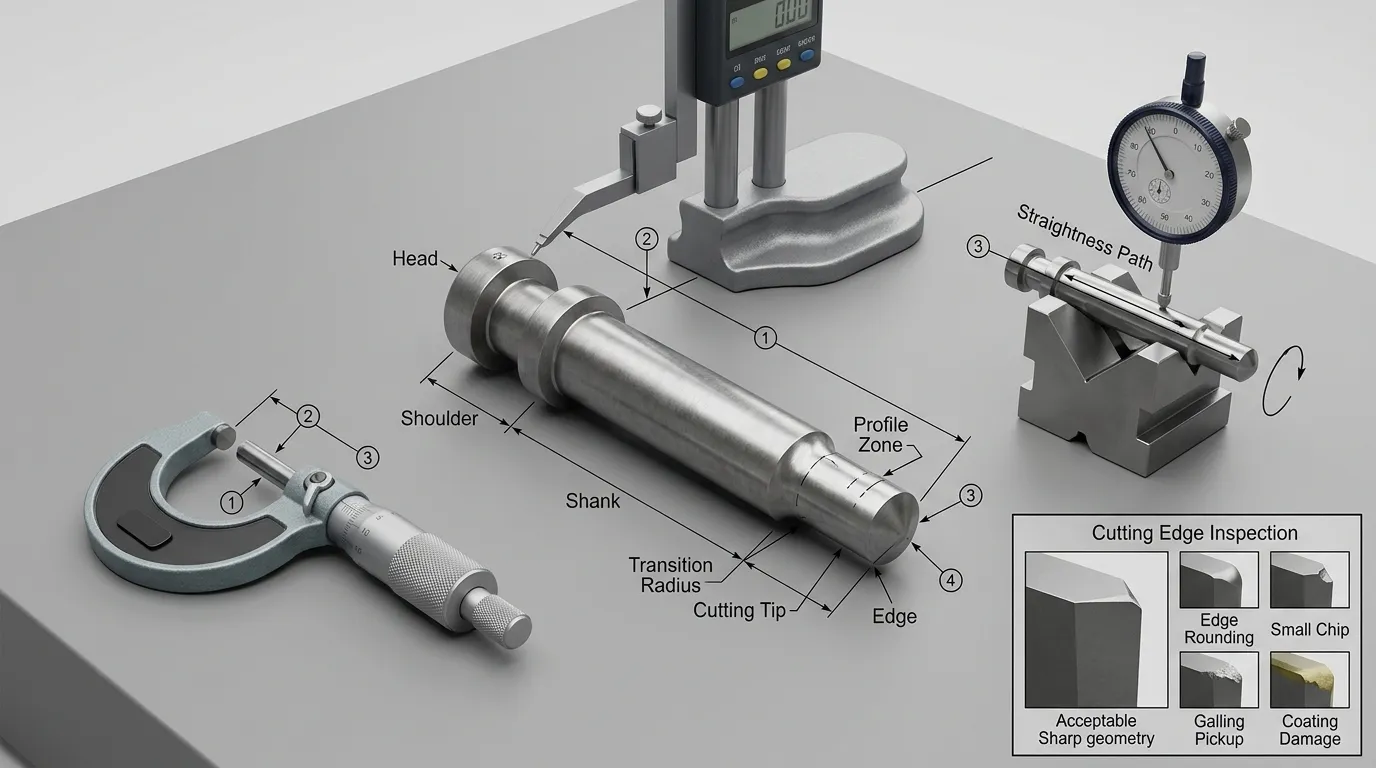
The approved drawing determines which dimensions and geometric controls must be inspected. Not every punch requires every measurement.
| 特徴 | なぜ重要なのか | 可能な測定方法 | 重大な制限 | 受理源 |
| ボディまたはシャンク直径 | Affects guidance, フィット感, 保持, およびアライメント | Outside micrometer; suitable limit gauge | 接触場所とテーパーを考慮する必要があります | 図面またはフィット仕様 |
| 先端直径 | 貫通特徴のサイズとパンチダイ関係に影響します | マイクロメーター, specialized gauge, optical system | 小さく繊細な先端は標準的なコンタクトには適さない場合があります | ドローイング |
| 形状先端のプロファイル | 非丸い穴や成形された形状の制御 | Optical comparator, vision system, CMM | 正確な基準合わせとプロファイル解釈が必要です | プロファイル要件付き図面 |
| 全長 | Supports identification, installation, and regrind tracking | Height gauge, micrometer, コンパレータ, dedicated fixture | 座席の面は清潔で、一貫して参照されている必要があります | ドローイング |
| 作業長または投影 | 作動位置と貫通への影響 | Height gauge, コンパレータ, dedicated inspection fixture | Definition must match the drawing; do not borrow tablet-tooling terminology | 図面またはセットアップ仕様 |
| ヘッド直径と厚さ | 定着率や座席数に影響を与える | マイクロメーター, caliper for screening, コンパレータ | バリやピーニングは接触を歪めることがあります | ドローイング |
| 肩の位置 | 座席と組み立てられた投影への影響 | Height gauge, コンパレータ, CMM | 基準設定は図面要件を再現しなければなりません | ドローイング |
| 直線性 | 曲げや軸のずれを検出します | Indicator with suitable support, CMM, dedicated fixture | 支持方法と基準面の選択が結果に影響を与えます | 引き出または承認されたサービス限度額 |
| 円形または全ランアウト | 基準軸に対する回転変化を示します | Indicator with centers or V-block; CMM | 「ランアウト」は描画制御と正確に一致しなければなりません | ドローイング |
| 同心率または同軸性 | 軸や特徴の関係を評価する | CMMまたは承認された特殊手法 | エンジニアリングの承認がない限り、単純なランアウトチェックを代替しないでください | ドローイング |
| 垂直性 | 座り方や端面・肩のアライメントに影響します | Indicator, surface plate setup, CMM | 有効な基準基準が必要です | ドローイング |
| 表面粗さ | Can influence friction, フィット感, リリース, and galling | 表面粗さ試験器 | パラメータ, cutoff, 演出, and location must be specified | 図面または表面仕様 |
| 硬度 | 熱処理の必要性が確認されるかもしれません | 承認された硬度試験またはサプライヤー文書 | Test scale, 所在地, 表面状態, and indentation effect matter | 図面または材料仕様 |
Geometric terms should be interpreted according to the drawing standard in use. ISO 1101 defines geometrical tolerancing concepts in the ISO system, ただし ASME Y14.5 is widely used for US-oriented GD&T drawings.
A drawing that specifies runout should not be rewritten as concentricity during inspection. These controls describe different requirements and may require different measurement strategies.
SunshinePro’s tungsten-carbide punch page lists micrometer or caliper checks, projector measurement, and roughness testing for that product category. Those published methods show the types of inspection that may be relevant, but they do not prove that every punch or every order receives the same checks.
公差と機能に基づいて楽器を選びます
Instrument choice should be based on the feature, 耐性, アクセス, and required measurement confidence.
| 楽器 | 最適な用途 | 主な制限 |
| マイクロメーター | アクセス可能な外径と厚さ | Contact geometry may not suit small, テーパード, delicate, or irregular features |
| キャリパー | Identification, broad dimensions, and screening | 解像度や演算子の影響は、厳密な公差には適さない場合があります |
| 高さ計と表面板 | Axial dimensions, shoulder positions, and comparative height checks | 座席と基準設定の管理が必要です |
| Vブロックまたはセンターを備えたダイヤルインジケーター | ランアウト, rotational variation, and some straightness checks | 結果は支持位置と基準面シミュレーションに大きく依存します |
| 光学比較器または視覚システム | Profiles, 角度, 半径, tip shapes, and edge form | Requires alignment, magnification control, and correct profile interpretation |
| CMM | 複素幾何学と基準面に基づく関係 | Probe access, 備具, strategy, and uncertainty must be controlled |
| ゴー/ノーゴーゲージ | サイズ制限の迅速な機能検証 | 合格・不合格情報は得られますが、実際の偏差や摩耗傾向は示していません |
| ラフネステスター | 数値表面テクスチャ検証 | Requires the correct parameter, 演出, cutoff, and measurement location |
プレーンリミットゲージは以下でカバーされます。 ISO 1938-1. A go/no-go gauge can be efficient for repeated checks, but variable measurement is still useful when the actual size or rate of wear matters.
Surface-texture requirements should be read from the drawing rather than inferred from appearance. ISO 21920-1 covers the indication of profile surface texture in technical product documentation.
結果が受け入れられるかどうかを判断してください
A measured value is not meaningful until it is compared with an approved requirement.
Possible acceptance sources include:
- the current approved drawing;
- the purchase specification;
- the control plan;
- an approved customer deviation;
- an approved sample with defined measurement criteria;
- a documented service limit;
- a validated internal wear limit.
Nominal size alone does not determine acceptance. A drawing dimension of 10 mm, 例えば, cannot be judged without its tolerance and any related geometric or surface requirements.
Use a controlled decision process:
| 結果条件 | 必須対応 |
| 明らかに要件の範囲内です | 結果を記録し、パンチを受け入れるか返品するかを選びます |
| 限界に近いか、不安定な状態 | Verify cleanliness, 温度, instrument, method, 備具, datum setup, and repeatability |
| 要件外 | パンチを隔離し、承認された不適合プロセスを開始してください |
| 仕様が欠落しているか、矛盾しています | 書面による説明が来るまでパンチは控えてください |
| 交換や再研磨後の繰り返しの欠陥 | より広いダイシステムとプロセス条件を調査してください |
Measurement uncertainty becomes important near a specification limit. ISO 14253-1 provides decision rules for proving conformity or nonconformity while accounting for measurement uncertainty.
In practical terms, a borderline reading should not be accepted or rejected casually. Confirm that the instrument and method are capable of resolving the requirement, then apply the organization’s documented decision rule.
サンプリングか100%検査かはリスクや契約要件によります
The inspection quantity should be determined by:
- customer or contract requirements;
- characteristic criticality;
- lot size;
- supplier performance history;
- process capability;
- failure consequence;
- previous nonconformities;
- whether the result is needed for wear trending;
- the control plan.
A statement such as “100% inspected” should identify which characteristics were checked. It may mean every punch received an identification and visual check, while only selected pieces received complete dimensional inspection.
Go/no-go gauging may support rapid inspection of every piece, but it does not provide the variable data needed to evaluate size distribution or wear trends.
故障前の摩耗を追跡するために定期的な点検を用いましょう
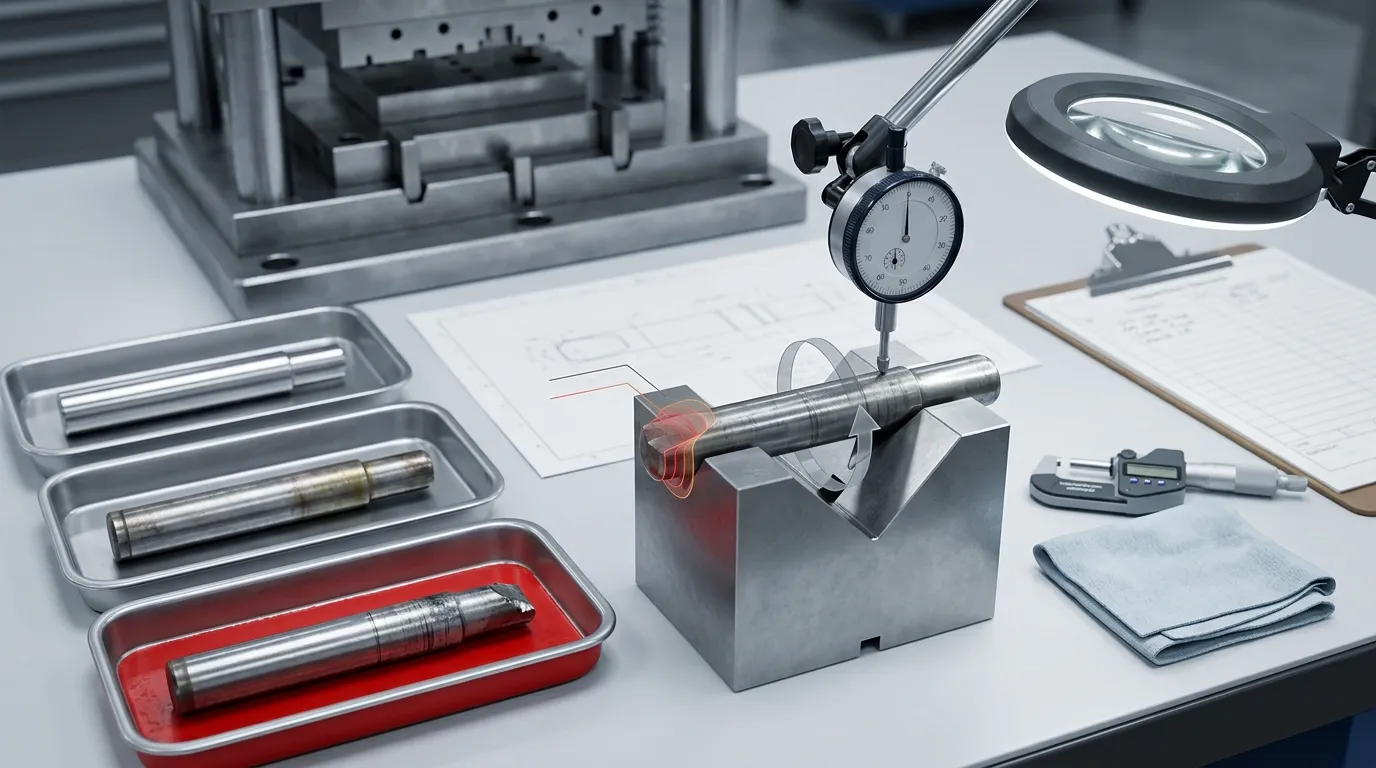
Routine QC should be based on risk and production history rather than one fixed interval for every punch.
Establish a baseline when the punch is first accepted, approved after setup, or returned from regrinding. Record dimensions and visible condition for the features most likely to change.
Trigger inspection when any of the following occurs:
- a planned production or maintenance interval is reached;
- the punch completes a high-risk or high-volume run;
- burr height or edge quality changes;
- stamped dimensions begin to drift;
- scratching or pickup appears on the part;
- stripping force increases;
- press load or operating sound changes;
- slug pulling or jamming occurs;
- a misfeed, collision, or material double-feed occurs;
- a nearby punch chips or breaks;
- the tool is removed for maintenance;
- 潤滑, stock material, or process settings change;
- the punch returns from regrinding.
Compare current values with the baseline and approved service limits. Trend data can reveal gradual wear before a dimension crosses a rejection limit.
Production symptoms should be treated as inspection triggers, not automatic diagnoses. Burrs may result from a worn punch, but they can also reflect die wear, クリアランス, アライメント, work-material variation, or stripper problems. その パンチダイズガイド provides broader context on die materials, 公差, クリアランス, and system-level tooling considerations.
再研磨や異常な出来事の後、パンチを再度確認してください
A sharp edge does not by itself prove that a reground punch is ready for service.
After regrinding, チェック:
- cutting-edge form;
- burr-free condition;
- 全長;
- working length or projection;
- tip diameter or profile;
- surface damage or overheating;
- remaining regrind allowance, where documented;
- identification and regrind history.
After a collision, misfeed, jam, or nearby breakage, also check:
- ひび割れ;
- permanent bending;
- head or shoulder deformation;
- ランアウト;
- 座席面;
- guide and retainer contact;
- the mating die opening and surrounding components.
Do not return a punch to service solely because no visible crack is present. A collision can change alignment or runout without producing an obvious surface defect.
結果を記録し、制御された処分を割り当てます
Inspection records should identify the punch, the requirement, the method, the result, and the final decision.
At minimum, 記録:
- 部品番号;
- 図面番号と改訂;
- supplier;
- purchase order;
- lot or serial number;
- material and coating designation;
- inspection stage;
- characteristic inspected;
- specification and tolerance;
- measured result;
- instrument identification;
- inspector;
- inspection date;
- disposition;
- 注記, photographs, or defect location where useful.
Use a controlled disposition rather than an informal “looks okay” decision.
| 発見 | 可能なレイアウト |
| すべての必要な特徴が適合しています | 受諾または復帰 |
| 結果は一貫性がなかったり、限界に近い | きれいだ, stabilize, remeasure, or verify with a more capable method |
| ドキュメントが抜けています | 証拠が提出されるまで拘束または隔離してください |
| 承認された許容範囲内で修復可能な刃の摩耗 | エンジニアリング承認の再研磨を依頼してください |
| パキッ, 深刻な欠け, permanent bending, or unsafe head damage | 置き換えか拒否するか |
| 次元は要件外です | 検疫と非準配法としての処理 |
| 同じダメージが繰り返し発生します | Investigate clearance, アライメント, ガイダンス, 保持, 潤滑, およびプロセス条件 |
Nonconforming punches should be clearly identified and physically segregated so they cannot return to production accidentally.
SunshinePro states that its quality approach includes raw-material inspection, プロセス中の監視, 最終試験, measuring equipment, and inspection reports. Buyers should still define the required inspection characteristics and documentation for each order rather than assume that one standard report fits every punch.
パンチピンのサプライヤーに依頼すべきこと
A buyer should define inspection evidence before the order is released, especially for custom or critical punches.
Request the items that are relevant to the application:
- 承認された図面と改訂;
- part, lot, and serial identification requirements;
- drawing-specific inspection report;
- material certificate or certificate of conformity;
- heat-treatment or hardness evidence where specified;
- coating documentation where specified;
- 承認された逸脱;
- packing and corrosion-protection requirements;
- identification of characteristics receiving 100% inspection;
- identification of characteristics inspected by sampling;
- measurement method for tight or complex tolerances;
- traceability between the punch, certificate, and inspection report.
Broad catalog statements are not a substitute for characteristic-level evidence. A supplier may state a general tolerance capability, but the buyer still needs confirmation that the required feature, 素材, 幾何学, and measurement method are suitable for the specific drawing.
SunshinePro lists tool steel, 高速鋼, カーバイド, CNC加工, 精密研削, EDM, 真空熱処理, and drawing-based customization on its punch-related pages. These published options can support an RFQ discussion, but the exact material, プロセス, 耐性, コーティング, and inspection documentation should be confirmed for the individual part.
パンチピン検査チェックリスト概要
Use this condensed sequence for incoming, routine, post-regrind, and post-event inspections:
- Identify the inspection stage.
- Confirm the part number, lot or serial number, 図面, and revision.
- Review the purchase order, control plan, and document requirements.
- Inspect packaging and record transport damage.
- Clean the punch without damaging its edge or coating.
- Verify instrument condition, 分布, 解決, and calibration status.
- Inspect the cutting edge, ヒント, ボディ, ヘッド, 肩, 半径, コーティング, and identification.
- Measure the dimensions and geometric characteristics required by the drawing.
- Use an instrument suitable for the feature and tolerance.
- Compare results with the approved acceptance source.
- Verify borderline results and account for measurement uncertainty.
- Record the specification, result, instrument, inspector, そして日付.
- Accept, hold, quarantine, regrind, 置き換え, or reject through a controlled disposition.
- Investigate the wider die system when the same damage repeatedly returns.
For a custom or replacement punch, submit the approved drawing together with the required material, コーティング, 検査, and documentation needs. サンシャインプロズ パンチピン page provides its published product context, および お問い合わせページ can be used to request drawing review or clarify inspection-report requirements.



サンシャインより書かれました
サンシャインで, 私たちは精密金型部品の専門製造およびサプライヤーです, プレスおよび射出成形用途向けの幅広い製品を提供しています. 私たちの主な焦点はパンチダイスです, イジェクターピンとスリーブ, ガイドポストとブッシング. 高度なCNC加工技術で, 厳格な品質管理, そして強力な生産能力, 私たちは信頼性を保証しています, 高精度部品, また、迅速かつ効率的なグローバル供給のための在庫の標準部品も併用しています.
ニュース
サービスを受けましょう
あらゆる予算に合った高品質な部品と、親切なスタッフが訓練されていて、訪問を有益で手間なく充実させてくれます.
