



タブレットパンチヘッドフラットとドウェルタイム: デザイン効果
A tablet punch head flat affects how long the punch remains at or near its maximum compression position beneath the main compression roller. At the same turret tangential velocity, a longer effective head flat generally produces a longer geometric dwell time. Increasing turret speed has the opposite effect.
That relationship is only the starting point. Actual tablet response also depends on compression force, roller geometry, press stiffness, and formulation behavior. A longer flat may help a strain-rate-sensitive formulation, but it does not automatically increase tablet strength or eliminate capping.
The head flat is one design feature within a complete tooling system. For broader punch, その, and tooling categories, 参照 タブレットプレスの金型タイプ.
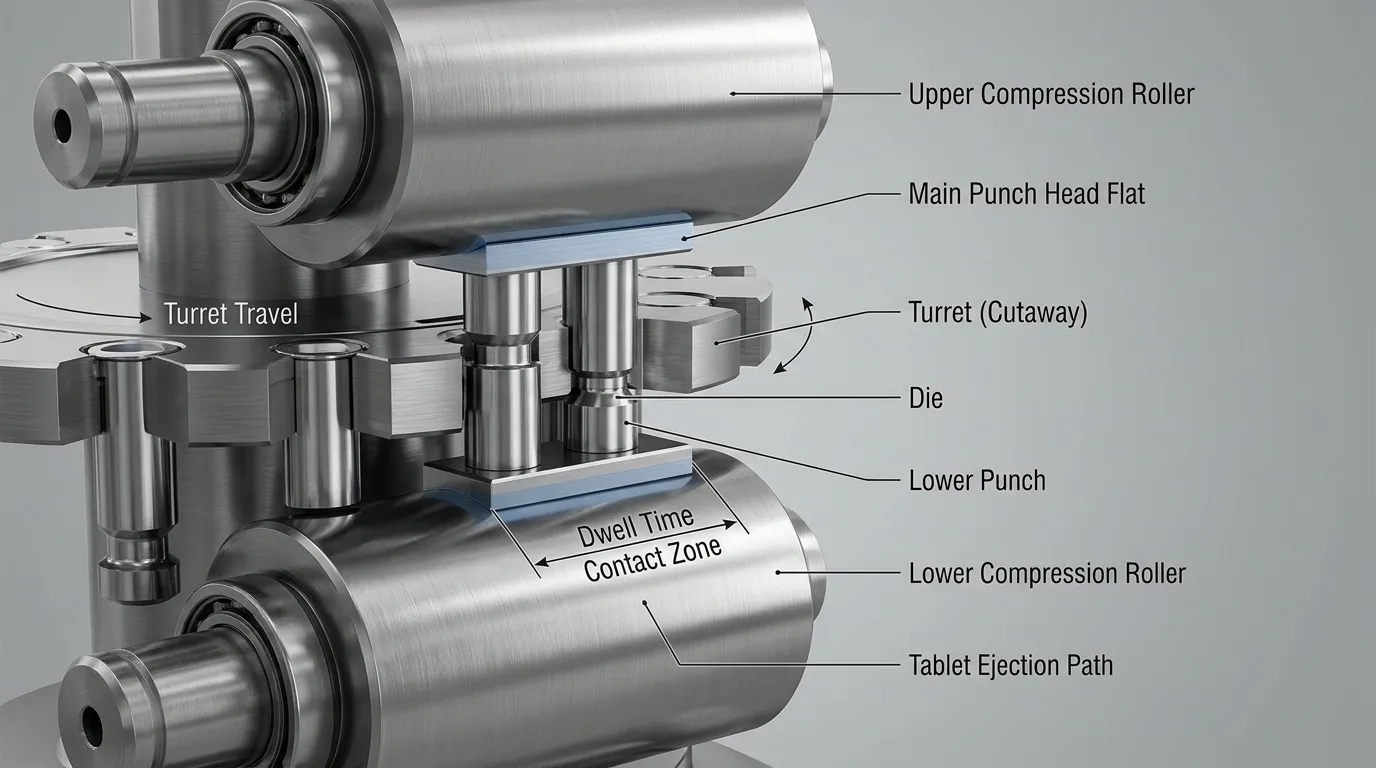
タブレット圧縮時にパンチヘッドがフラットに変えるもの
On a rotary tablet press, the upper and lower punch heads pass between the main compression rollers. As the rollers act on the punch heads, the punch tips move into the die and compact the powder bed.
The head flat is the relatively level section of the punch head that travels beneath the roller at the maximum-compression region. Its relevant dimension is the effective length in the direction of turret travel.
A longer effective flat keeps the punch near its minimum separation from the opposing punch for a greater travel distance. At an unchanged linear speed, that increases calculated dwell time.
This geometry is separate from the tablet-forming end of the punch. カップ戦の深さ, スコアライン, logos, and other face details belong to punch-tip design. Those adjacent decisions should be handled through separate タブレットエンボス設計ガイドライン.
Geometric Dwell, Force-Based Dwell, and Consolidation Time Are Not Identical
その言葉 居住 is not always used in the same way.
| 用語 | 記述内容 | 主な変数 |
|---|---|---|
| 幾何学的滞留時間 | 最大圧縮領域を通過するパンチヘッドのフラットな時間の計算時間 | 有効フラット長と接線速度 |
| 力に基づく滞留時間 | 測定された圧縮力プロファイルからドウェルが特定されます | 幾何学, force level, formulation response, and measurement definition |
| 統合時間または圧縮時間 | 火薬床が圧縮される負荷イベントのより広い部分 | Roller profile, punch-head geometry, 速度, displacement, and press behavior |
2024年の査読付き研究 力に基づく滞留時間と幾何学的滞留時間 found that measured dwell can vary with compression force and formulation even when the press geometry remains fixed.
For that reason, a geometric calculation is useful for equipment comparison and initial design work, but it should not be treated as a complete description of the tablet’s force-time history.
幾何学的停留時間の計算方法
A simplified geometric dwell calculation uses:
[
t = \frac{L}{v}
]
ここで:
- (t) = geometric dwell time
- (L) = effective head-flat travel length
- (v) = tangential velocity at the punch position
Tangential velocity can be estimated from turret pitch circle diameter and rotational speed:
[
v = \frac{\pi \times PCD \times RPM}{60}
]
When PCD is expressed in millimetres, the result is millimetres per second. Dwell time in milliseconds is then:
[
t_{ms} = \frac{L}{v} \times 1000
]
図示的計算
Assume:
- Effective flat length: 10mm
- Turret PCD: 400 mm
- Turret speed: 30 RPM
Tangential velocity:
[
v = \frac{\pi \times 400 \times 30}{60}
]
[
v \approx 628.3\text{ mm/s}
]
Geometric dwell:
[
t = \frac{10}{628.3} \times 1000
]
[
t \approx 15.9\text{ ms}
]
This is an illustrative calculation, not a recommended dwell target. The actual tooling drawing, press geometry, roller arrangement, and operating conditions must be used for engineering decisions.
Use Effective Travel Length, Not a Generic Head Diameter
The complete punch-head diameter is not necessarily the correct dimension for dwell calculations.
For a round flat, the useful measurement is the flat dimension along the direction of turret travel. For an oval or elliptical flat, the long axis may be aligned with the travel direction to create more dwell without increasing the head equally in every direction.
The calculation should therefore use the effective travel length shown on the tooling drawing, not a generic head diameter taken from a catalogue or another press.
This distinction becomes especially important when comparing:
- 標準的な丸型フラット
- 拡張された円形フラット
- 楕円形または楕円形のフラット
- 指向性またはキー付きヘッド設計
- 短時間居住条件に使われる縮小フラット
なぜRPMだけでは2台のタブレットプレスを比較できないのか
Two presses operating at 30 RPM can produce different dwell times if their turret pitch circle diameters differ.
A larger PCD means the punch travels a greater linear distance during each turret revolution. At the same RPM, it therefore has a higher tangential velocity and passes beneath the compression roller more quickly.
Press comparison should use at least:
- 砲塔回転数
- ピッチサークル直径
- 有効ヘッドフラット長
- 圧縮ロール形状
Comparing RPM alone can create a false impression that development and production presses are operating under equivalent compression conditions.
ヘッドフラット設計の選択肢とそのデビルのトレードオフ
The appropriate head-flat design depends on the required dwell, press geometry, 工具規格, mechanical support, and formulation response.
| ヘッドフラット設計 | 滞留効果 | 潜在的な利点 | 主な制限 |
| 標準的なドーム型ヘッド | プレスおよび工具構成の基準停留時間 | 従来型互換性と確立された運用 | 高度にレート感応的な配合には滞留時間が不足する場合があります |
| エクステンデッドラウンドフラット | 実効的な移動距離を増加させる | 砲塔速度を落とさずにより長い幾何学的停留 | 周囲のヘッド形状が狭くなったり、クリアランスや応力の問題を引き起こす可能性があります |
| 楕円形または楕円形の平ら | 主に一方向に移動距離を増やします | 制限されたヘッド幅内でより多くのドウェルを作り出せます | May require keying, orientation control, and additional wear assessment |
| 縮減フラット | 有効移動距離を短縮する | 現像印刷機が短い生産時間を再現するのに役立ちます | 最大圧縮時の持続時間短縮と、動作余裕の狭さ |
スタンダードおよびエクステンデッドラウンドフラット
A standard domed punch head includes a flat surrounded by curved transition geometry. It provides the baseline dwell associated with the press speed, turret PCD, and standard tooling dimensions.
An extended round flat increases the flat region. At the same tangential velocity, this increases geometric dwell without slowing the turret.
The trade-off is that the flat cannot be enlarged without considering the rest of the head. Increasing it may reduce the available crown, outside radius, ヘッド厚み, or support above the punch neck. The design must still carry the compression load and pass safely through the press.
Oval, Elliptical, and Reduced Flats
An oval or elliptical head flat extends the contact path in the direction of turret travel while limiting growth across the head width. This can be useful where a full circular extension would interfere with surrounding press geometry.
Because the long axis must remain aligned with the travel direction, directional heads may require keyed tooling. Keying adds orientation control but can also affect interchangeability, setup, and localized wear.
A reduced flat serves the opposite purpose. It can shorten geometric dwell when a laboratory or development press naturally provides a longer dwell than the intended production machine.
Dwellが製剤挙動やタブレット品質とどのように相互作用するか
Head-flat geometry creates a time opportunity. The formulation determines what happens during that time.
Tablet materials can respond through several mechanisms:
- 塑性変形: Particles change shape permanently, increasing contact area and supporting interparticle bonding.
- Elastic deformation: Particles recover after the load is removed, which can reduce retained bonding and increase residual stress.
- Viscoelastic behavior: Deformation depends on both time and loading rate.
- Brittle fragmentation: Particles fracture and create new bonding surfaces.
A slower loading event or longer dwell may support additional plastic flow in some formulations. Other materials may show little improvement, or the benefit may depend strongly on pressure, 潤滑, 水分, particle size, and previous processing.
研究 タブレット圧縮中の長時間停留 shows that material behavior must be evaluated under controlled conditions rather than predicted from head geometry alone. Earlier work on paracetamol and microcrystalline cellulose also found that dwell effects were linked with pressure history, recovery, and energy, not simply with a longer period beneath the roller.
なぜ長時間の停留が強い錠剤を保証するわけではないのか
Tablet strength depends on more than dwell. Relevant variables include:
- 圧縮圧力
- 粒子変形機構
- 粉床間隙率
- 潤滑剤濃度と混合
- 含水率
- 弾性回復
- 積み込みおよび荷降ろし速度
- プレ圧縮条件
A longer head flat may increase geometric dwell while the measured force plateau changes only slightly. 逆に, two formulations running with the same tooling may produce different force-based dwell profiles.
Breaking force and tensile strength also should not be treated as identical. Breaking force is a measured load, while tensile-strength calculations account for tablet dimensions and provide a more normalized comparison.
キャップとラミネーションは多因子の問題です
Capping and lamination are sometimes associated with inadequate dwell, but increasing the head flat is not a universal correction.
Possible contributors include:
- 粉床に空気が閉じ込められている
- 急速な力の加護
- 不均一な密度
- 過剰弾性回復
- 不十分または過剰な前圧
- 定式化または粒化特性
- 潤滑条件
- 急速減圧
- 工具の状態またはアライメント
査読付き調査 強制適用率と錠剤の上限 identified interactions among loading rate, 空気が閉じ込められている, densification, and viscoelastic recovery.
Additional dwell may help a specific formulation, but it should be tested as one process variable within a broader root-cause study.
パンチヘッドを平らに伸ばす前の機械的限界
A longer flat must remain mechanically sound and compatible with the press. The maximum useful flat is not determined by dwell requirements alone.
| 設計上の問題 | 可能な結果 | 検証が必要です |
| パンチネックのサポート不足 | Head deflection, 応力集中, or premature failure | ネック直径および遷移形状の構造的レビュー |
| 外頭半径の縮小 | 局所的な接触応力が高まる | ヘッドプロファイルとローラーコンタクトの評価 |
| 過剰なヘッド幅または長さ | カムトラックや隣接するプレス部品との干渉 | プレスパスクリアランスの完全なチェック |
| 方向性楕円形状 | ローラー下の誤った向き | キーイングおよび向き制御のレビュー |
| 小または高負荷の接触領域 | Pitting, 表面疲労, または不均一な摩耗 | 接触応力と材料評価 |
| ヘッドの厚さが不一致 | カムや圧縮ステーションを通る不適切なトラベル | OEMと工具標準の比較 |
| 未検証のロール相互作用 | 変化した力の加因やエッジ荷重 | 圧縮ロール直径とプロファイルレビュー |
Head Strength, Neck Support, and Contact Wear
The punch neck supports the head during compression. Extending the flat can reduce the surrounding curved geometry that transfers force from the roller into the neck.
Critical features include:
- ネック直径
- ヘッド厚み
- 遷移半径
- 外頭半径
- 接触体位
- 材料および熱処理の状態
A sharper or smaller outside radius can increase contact stress between the head and compression roller. Repeated loading may then contribute to pitting, 表面疲労, または不均一な摩耗.
These effects require engineering analysis for the actual punch and press. Generic maximum-flat dimensions should not be applied across different tooling standards or machine models.
Cam Tracks, Roll Geometry, and Keyed Orientation
The head must pass through the complete cam path, not only the main compression station. A design that works beneath the roller can still interfere with entry cams, exit cams, lifting tracks, or other press components.
Non-round flats add an orientation requirement. If the long axis must remain aligned with turret travel, a key or another rotation-control feature may be necessary.
Compression-roll geometry also matters. Roller diameter and profile influence the loading path before and after the nominal dwell region. A head-flat change therefore should be reviewed with the actual roll arrangement rather than evaluated as an isolated component.
スケールアップおよびプレス転送時のマッチングドウェル
Dwell comparison is often used when transferring a tablet from a development press to a production machine.
A useful comparison should collect:
- 砲塔ピッチ円径
- 動作回転数範囲
- 有効上および下部パンチヘッドフラット寸法
- メインおよびプレ圧縮ロールジオメトリ
- 圧縮力の範囲
- 錠剤の厚さと寸法
- プレ圧縮条件
- 製剤ひずみ率感度
- 利用可能な場合はプレス剛性や変形データ
- 測定された力と変量プロファイル
The first calculation should compare tangential velocity and geometric dwell. It should then be checked against tablet properties and measured compaction behavior.
原理 ICH Q8(R2) Pharmaceutical Development support building process understanding around material attributes and process parameters rather than relying on one isolated setting.
Dwellのマッチングは、完全な圧縮イベントをマッチングすることとは異なります
Two presses can have similar geometric dwell but different:
- 積載速度
- ローラー半径
- 最大力
- 変位プロファイル
- プレス変形
- プレ圧縮履歴
- 減圧率
- ダイ充填条件
Matching dwell therefore does not guarantee identical tensile strength, porosity, dissolution behavior, or defect risk.
A compaction simulator can help reproduce selected force and displacement profiles under controlled conditions. It is useful for studying formulation sensitivity and planning scale-up, but production-press verification is still required.
Which Adjustment Should Be Used to Change Dwell Conditions?
The best intervention depends on the problem being solved.
| 調整 | 最適な使用例 | 利点 | 制限 |
| 砲塔速度を落とす | 配合がレートに敏感かどうかのテスト | 単純なプロセス試験 | 出力を減らし、他のプレス条件を変えることもあります |
| ヘッドを伸ばしたり形を変えたりする | より多い幾何学的停留が必要であり、標準的な砲塔速度は低下しません。 | 速度の可能性を維持 | 新しいツールと完全な互換性レビューが必要 |
| 圧縮ロールジオメトリの変更 | より広い統合プロファイルは調整が必要です | 積み込みや荷降ろしの挙動を変えることができる | プレスに依存し、機械の改造が必要な場合があります |
| 圧縮シミュレーターを使いましょう | 開発やスケールアップの条件は管理された評価が必要です | 繰り返し可能な力プロファイルの研究を可能にします | 生産検証の代わりにはなりません |
| 配合や予圧縮の調整 | The root cause is material behavior, air, 潤滑, or densification | 根本的なメカニズムに対処します | 製薬開発と変更管理が必要 |
A practical sequence is to test speed sensitivity first, because a controlled speed reduction can show whether more time under compression improves the formulation. If it does, engineers can evaluate whether modified head geometry, different roll conditions, or formulation work offers the most suitable production solution.
異なるヘッドフラットを指定する前に確認すべきデータ
A request for “more dwell” is not enough for a tooling designer. The specification should include:
- タブレットプレスのメーカーとモデル
- 適用される工具規格
- 現在の上部および下部パンチ図面
- 既存のヘッドフラット寸法
- 望ましい有効進行方向
- 砲塔ピッチ円径
- 通常回転数と最大動作回転数
- メインおよびプレ圧縮ロールの詳細
- 圧縮力の範囲
- カムトラッククリアランス情報
- パンチネック寸法
- キーイングまたは回転制御の要件
- タブレットの寸法とターゲット特性
- 開発および制作プレスデータ
- 製剤感受性または圧縮研究結果
- 検査およびトレーサビリティの要件
- 提案された検証方法
Current dimensional requirements should be checked against the applicable standard and press documentation. The American Pharmacists Association’s タブレット仕様マニュアル is a current North American reference for tablet-tooling terminology, 設計, and interchangeability. Other tooling systems may require different standards and OEM requirements.
プレスOEMや金型サプライヤーに尋ねるべき質問
Before approving a modified head, 確認してください:
- Will it pass safely through every cam track?
- Does the punch neck provide enough structural support?
- Will the head contact the compression roll as intended?
- Does the design require a key or controlled orientation?
- Which current standard governs the dimensions?
- How will flat length, プロフィール, and orientation be inspected?
- What contact-stress or wear evaluation is required?
- Will the tooling remain interchangeable with existing sets?
- How should the new design be validated on the intended press?
- What material, 熱処理, コーティング, and traceability documentation will be supplied?
ヘッドフラットな変更を制御された工学的判断として活用しましょう
Tablet punch head flat and dwell time are directly related at the geometric level: a longer effective flat increases dwell when tangential velocity remains unchanged. That calculation is useful, but it does not predict tablet performance by itself.
A defensible design decision combines geometric dwell, measured compaction behavior, formulation response, 機械的強度, cam compatibility, roll geometry, and current tooling requirements. Calculate first, test the formulation, verify the press constraints, and compare alternative interventions before approving a modified punch head.
共有:



サンシャインより書かれました
サンシャインで, 私たちは精密金型部品の専門製造およびサプライヤーです, プレスおよび射出成形用途向けの幅広い製品を提供しています. 私たちの主な焦点はパンチダイスです, イジェクターピンとスリーブ, ガイドポストとブッシング. 高度なCNC加工技術で, 厳格な品質管理, そして強力な生産能力, 私たちは信頼性を保証しています, 高精度部品, また、迅速かつ効率的なグローバル供給のための在庫の標準部品も併用しています.
ニュース
サービスを受けましょう
あらゆる予算に合った高品質な部品と、親切なスタッフが訓練されていて、訪問を有益で手間なく充実させてくれます.
