



信頼性の高い分割と工具寿命のためのタブレットブレークライン設計
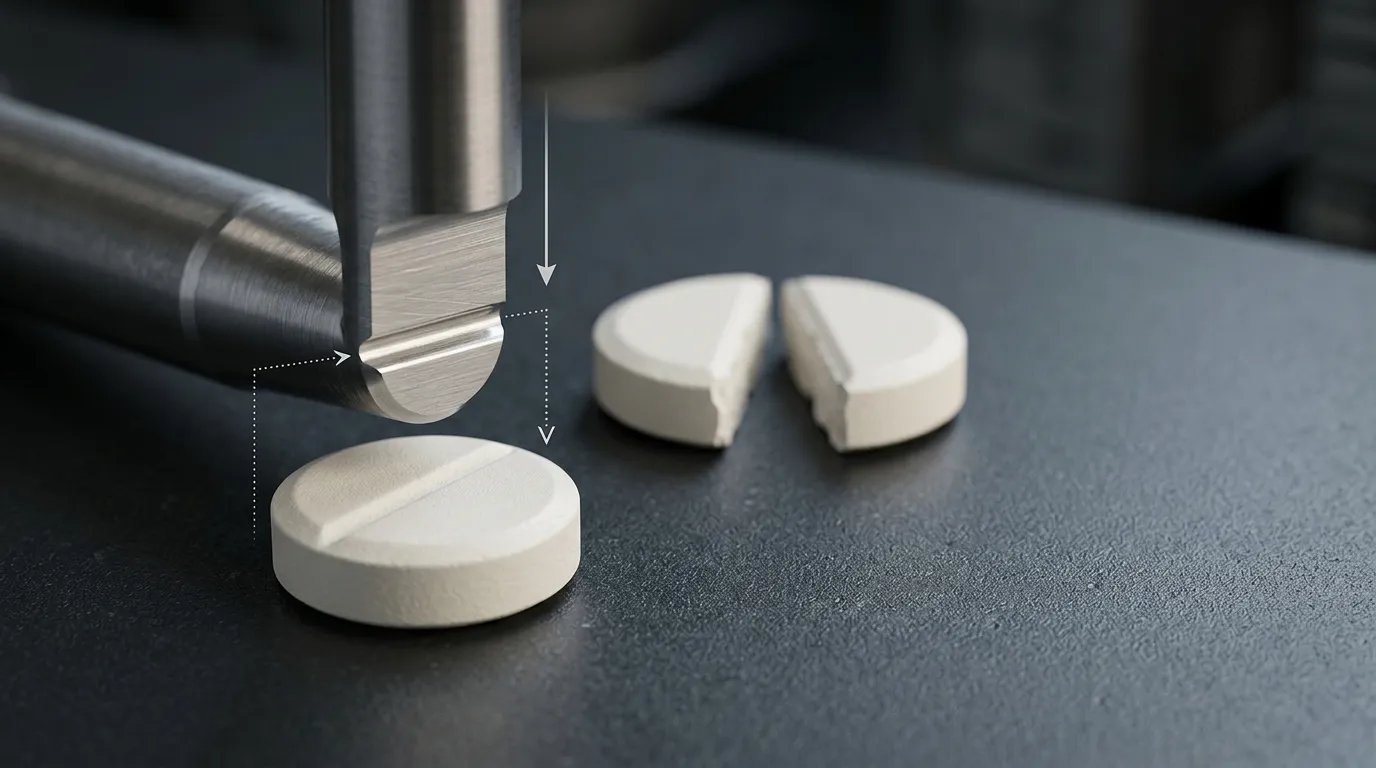
Tablet break line design is not a matter of making the deepest possible groove. A functional break line, also called a tablet score line, must guide the tablet along an intended fracture path while leaving enough strength for compression, 射出, コーティング, パッケージング, およびハンドリング.
The geometry must also be practical for the punch tip that forms it. A sharper or more protruding feature may help initiate a break, but it can increase local stress, reduce clearance between upper and lower punches, or make the tooling more vulnerable to chipping.
ブレークラインジオメトリは、より広い範囲の中の一つの専門的な決定です。 タブレットプレスの金型タイプ. The final design should be evaluated as a system involving the tablet shape, 厚さ, 定式化, 硬度範囲, punch configuration, プレスセットアップ, and product-validation method.
What Makes a Tablet Break Line Functional?
A functional score line is intended to help a tablet divide into defined portions. Its performance cannot be judged only by how visible, straight, or symmetrical the groove appears.
A useful break line should support several outcomes:
- The tablet can be held and divided using the intended method.
- Fracture occurs close to the planned path.
- The resulting portions are reasonably consistent.
- Material loss from crumbs and fragments remains controlled.
- The intact tablet remains strong enough for production and handling.
- Subdivision does not create unacceptable changes in product performance.
ザ FDAの錠剤評価に関する指針 treats scoring as a product-performance issue rather than a cosmetic feature. Depending on the product and market, evaluation may include splitting behavior, mass loss, もろさ, 解散, 安定性, and performance across the proposed tablet-hardness range.
機能スコアと装飾溝の比較
A tablet may contain a visible groove without being suitable for accurate subdivision. A decorative line may improve appearance or product recognition, but it should not be represented as a functional score unless the finished tablet has been tested for that purpose.
Visual inspection can confirm that the groove exists. It cannot prove that:
- The fragments have consistent mass.
- The active ingredient is evenly distributed.
- The tablet will divide similarly across the production hardness range.
- The split portions retain acceptable release characteristics.
- Patients or operators can reproduce the result using the intended method.
Tooling inspection and tablet-performance validation are therefore separate requirements.
折れ線ジオメトリ変数とそのトレードオフ
A score feature is defined by several connected dimensions. Changing one variable can affect the others, so break-line depth should never be specified in isolation.
| 設計変数 | 意図された効果 | やりすぎるとリスクがあります | 検証すべきこと |
|---|---|---|---|
| 深さまたは貫通 | 破損しなければならない錠剤部分を減らす | Weak intact tablet, fragile center, tall punch feature | Tablet strength, split force, punch clearance |
| 溝幅 | スコアのスペースを作り、そのプロフィールに影響を与えます | 過剰な素材の除去や視覚の不明確さ | 破壊挙動と製造可能性 |
| 含まれる角度 | 破壊経路を集中させる | 鋭いパンチジオメトリと高い局所応力 | パンチの強さと細分化の一貫性 |
| 根半径 | スコアの下部のシャープネスを制御します | Too small may weaken the tooling; too large may reduce fracture guidance | 工具の応力とタブレットの破損性 |
| 楽譜の長さ | 誘導破壊経路を延長します | エッジの欠けや他の特徴との干渉 | 亀裂経路とタブレット面の配置 |
| 位置と方向 | 意図されたセグメントジオメトリを定義します | 不均等な断面やずれ | Symmetry, キーイング, and drawing orientation |
The correct combination depends on the tablet rather than on a universal score-line standard.
深さ, Width, and Remaining Tablet Section
A deeper groove leaves less tablet material beneath the score. This can reduce the force needed to start a fracture, but it can also weaken the tablet before the user intends to split it.
Depth must be considered relative to:
- Overall tablet thickness.
- Cup depth and face curvature.
- The location of the score across the curved surface.
- Tablet hardness.
- Whether the opposite face also contains a score.
- The height and shape of the punch-tip feature.
例えば, the same nominal score depth may leave a substantial residual section in a thick, shallow-profile tablet but a much thinner section in a smaller tablet with a deep cup.
Groove width also affects the feature profile. It should provide a manufacturable transition without removing more material than necessary or creating a punch feature that is too thin to withstand repeated loading.
角度と根半径
The included angle and root radius influence how strongly the score concentrates stress when the tablet is bent.
A sharp groove can encourage fracture to start at the intended line. The corresponding punch-tip feature, しかし, may contain a thin or sharp transition where mechanical stress becomes concentrated during each compression cycle.
A larger root radius generally creates a smoother tooling transition, but it may provide less concentrated fracture guidance in the tablet. This is why angle and radius should be reviewed together rather than treated as independent cosmetic dimensions.
技術的なタブレット設計のソースとしては I Holland タブレットデザイン用紙 discuss score penetration, 半径, 角度, punch stress, and the need to balance tablet breakability with robust tooling. These relationships are useful design principles, but they do not establish a universal dimension for every formulation.
長さ, 位置, and Interaction With Face Features
The score should follow the intended segment boundary and remain compatible with the tablet’s shape and face profile.
Its endpoints require particular attention. A line that extends too close to a tablet edge may create a vulnerable edge condition, while a line that stops too early may not guide the complete fracture path.
Other face features also affect placement:
- Logos and characters can interrupt a symmetrical fracture path.
- Deep embossing can compete with the score for available face area.
- Curved surfaces can change the effective score penetration along its length.
- Off-center placement can create unequal tablet sections.
- Multiple intersecting scores increase both tablet and punch-tip complexity.
The score, identification marks, and overall cup profile should be reviewed as one punch-face layout.
なぜタブレットの性質が結果を変えるのか
Identical punch geometry can produce different subdivision behavior in different formulations.
Tablet size and shape influence how the product can be held and where bending forces are applied. A large oblong tablet may provide more leverage than a small round tablet, even when the score geometry appears similar.
Thickness and cup profile determine how much material remains under the groove. Formulation properties then control how that material responds to stress.
Relevant formulation behavior includes:
- 脆さ.
- 弾性回復.
- 塑性変形.
- Compactability.
- Internal bonding strength.
- Distribution of the active ingredient.
Compression force also changes the result because it influences tablet density and hardness. A score that performs well at one development condition may become difficult to break at a higher hardness or excessively fragile at a lower one.
査読付きレビュー Tablet Scoring: Current Practice, Fundamentals, and Knowledge Gaps describes tablet subdivision as a multivariable problem involving patient use, タブレットの幾何学, 定式化, manufacturing conditions, and the selected test method.
The design should therefore be evaluated across the intended production range, not only on a single batch produced under ideal development conditions.
Single-Sided or Double-Sided Scoring?
A tablet can be scored on one face or on both opposing faces. Neither configuration is automatically better.
| 選択係数 | 一方的なスコア | 両面得点 |
| パンチ構成 | ワンパンチフェイスにスコア機能 | 上部と下部パンチの協調した特徴 |
| 回転アライメント | 通常はそれほど負担が少ないです | 対立する特徴は整列し続けなければなりません |
| 残存するタブレットセクション | 一方から制御 | 両陣営から縮小 |
| クリアランスリスク | 無得点の相手面は下がる | 対向突起はパンチチップの隙間を減らすことができます |
| 面配置の複雑さ | 反対側の面を空けておく | 両面のスペースを使います |
| セットアップ感度 | 一般的にはよりシンプルです | キーイングや名目長により依存します |
| 検証の必要性 | 製品別 | 積- and setup-specific |
A double-sided score may guide fracture from both surfaces, but it introduces additional mechanical and setup requirements. The two features must be positioned correctly relative to each other, and their combined penetration must not leave an excessively weak central section.
The choice should be based on the tablet geometry, 定式化, intended segment pattern, available face area, 工具システム, and validation results.
対立スコアのアライメントとキーイング
Opposed score features must remain rotationally aligned during production. If one punch turns relative to the other, the score lines may no longer meet across the intended fracture plane.
Anti-turn keys and key guides can control punch orientation. Depending on the tooling arrangement, the lower punch may also require a keyed configuration.
The review should confirm:
- Which punch faces contain the score.
- The required angular orientation.
- The location of each key.
- Whether the press supports the intended keyed arrangement.
- How orientation will be checked during setup.
- Whether key or guide wear could allow movement over time.
This discussion is limited to score alignment. General upper- and lower-punch functions belong to the broader tooling system rather than this specific break-line decision.
パンチチップの接触や早期故障から保護する方法
The score feature machined into a punch face may be narrow, sharp, or raised relative to the surrounding cup. These conditions can increase local mechanical stress.
Repeated compression subjects the punch to cyclic loading. A geometry with a thin section or abrupt transition may become more vulnerable to fatigue, while an overload, contact event, unsuitable material condition, or handling impact can contribute to chipping or brittle fracture.
ある 製薬技術における工具の故障に関する議論 identifies fatigue, brittle fracture, パンチ設計, 材料の状態, and compaction load as relevant contributors to punch-tip damage.
The main tooling risks associated with a break line include:
| リスク | 可能な原因 | 可能な結果 | レビューの行動 |
| 局所応力集中 | Sharp angle, small radius, thin feature | 疲労割れやチップスコア機能 | トランジションとロードのレビュー |
| 対立特徴接触 | 上下クリアランス不足 | 即時の欠けや破損 | 公称の長さと先端の隙間を確認してください |
| 回転のずれ | キーイングまたはセットアップの問題 | Uneven score, 干渉, poor fracture path | 向き制御の検証 |
| 過剰特徴突出 | ディープスコアジオメトリ | 射出干渉またはクリアランスの低下 | 機能高さとタブレット除去のレビュー |
| 過負荷 | 高い圧縮力または異常なプレス状態 | 塑性変形または脆性破壊 | 作動範囲を確認する |
| マージナルタブレット設計 | 過剰な貫通や弱い中央部分 | 早期の錠剤骨折 | 生産条件を横断した試験 |
Tool material and heat treatment affect durability, but they cannot compensate for direct punch contact, an unsafe stress concentration, or an incorrect press setup.
サンシャインプロズ タブレットプレスの工具ページ 高速鋼の一覧, CNC加工, 熱処理, 寸法検査, and custom tooling from drawings or samples. These are relevant supplier capabilities, but they should not be interpreted as a guarantee of score performance or tool life for a specific product.
上から下へのパンチクリアランス
Double-sided or highly protruding score features require careful clearance review.
The available gap depends on more than the visible tablet thickness. It can also be affected by:
- Feature height above each punch face.
- Upper and lower punch nominal lengths.
- Compression position.
- Press adjustment.
- 工具の摩耗.
- Setup error.
- Deflection under load.
A practical review sequence is:
- Dimension the score features on both punch drawings.
- Confirm the nominal lengths of the upper and lower punches.
- Calculate the minimum expected separation at the operating position.
- Include a suitable safety margin for manufacturing and setup variation.
- Verify the arrangement during installation and trial compression.
- Inspect the punch tips after the trial for evidence of contact.
Press-specific values should come from the press manufacturer, approved tooling drawings, and project calculations rather than from a generic article.
スコアに関連する制作および取り扱いの問題
A scored tablet can survive compression but fail during a later production stage.
射出時, the lower punch raises the tablet through the die. A weak score area may chip as the tablet moves, while a protruding punch feature may complicate release from the punch face.
Take-off introduces another contact event. If the tablet has already been weakened excessively, lateral movement can cause edge damage or premature fracture.
Coating and packaging can also expose a marginal design:
- Coating may bridge across the groove.
- Coating film may crack when the tablet is divided.
- Tablets may rub against each other during coating and handling.
- Packaging equipment may apply local loads.
- Transport vibration may break tablets that lack sufficient intact strength.
These problems do not prove that the score is always the root cause. The formulation, ejection force, 工具の状態, コーティング工程, packaging design, and handling system may also contribute.
The purpose of the break-line review is to determine whether the score has created an avoidable weak section or tooling feature before wider process changes are made.
ブレーキラインを交換する前に故障を診断してください
A score redesign should follow evidence, not assumptions.
| 観測された問題 | 可能な原因 | 収集すべき証拠 |
| タブレットは分割が難しい | Shallow score, high hardness, unsuitable formulation, poor grip, unsuitable test method | Hardness data, breaking method, segment results |
| タブレットがスコアから離れる | Misplaced line, formulation fracture pattern, asymmetric geometry | Fracture location, cross-section, タブレットの寸法 |
| 不等分断片 | Off-center score, rotational misalignment, inconsistent splitting method | Tool orientation, segment mass, user method |
| 排莢時のタブレットチップ | Weak edge, excessive penetration, high ejection force, 工具の状態 | Ejection data, chip location, punch and die inspection |
| タブレットがキャップに分離します | 空気の閉じ込め, formulation or compression issue, tooling configuration | Defect plane, press parameters, formulation review |
| パンチスコアのフィーチャーチップ | Direct contact, 応力集中, 過負荷, 損傷の取り扱い | Tip-gap check, fracture surface, setup records |
Capping should not be treated as another name for a score-related break. A score is intended to guide fracture through a defined plane, while capping usually involves separation of the top or bottom portion of the tablet from the main body.
Where the defect pattern indicates cap separation rather than failure along the intended score, the reader should move to the dedicated タブレットキャッピングツールソリューション guidance instead of expanding the break-line article into a full capping investigation.
機能的なブレークライン設計の検証方法
A functional break line requires verification at several levels. Dimensional inspection alone is not enough.
1. Inspect the Tooling
Confirm that the manufactured punches match the approved drawings.
Relevant checks may include:
- Score depth.
- Width.
- 含まれる角度.
- 根半径.
- Length and endpoint position.
- 向き.
- キーポジション.
- Upper and lower punch nominal lengths.
- 地表の状態.
- Opposed-feature clearance.
SunshineProは寸法検査および検査報告を説明しています。 品質管理の実践. These checks can verify whether the tool conforms to the specification, but they do not establish how a pharmaceutical formulation will behave.
2. Conduct Representative Press Trials
Trials should use the intended formulation and a relevant operating window.
The trial plan should consider:
- Low and high tablet-hardness conditions.
- Expected compression-force range.
- Production speed where it affects performance.
- Ejection and take-off behavior.
- Tool orientation.
- Evidence of upper/lower punch contact.
- Tablet chipping or premature fracture.
- Repeated-cycle effects on the punch feature.
A single successful compression event does not prove that the design is robust for production.
3. Evaluate the Whole Tablet
Before subdivision, confirm that the scored tablet remains suitable for handling.
Evaluation may include:
- Visual integrity.
- Breaking force or hardness.
- Friability.
- Resistance to coating and packaging damage.
- Stability during normal storage and transport.
- Consistency across batches and operating conditions.
The score should not make the intact tablet so weak that it breaks before the intended use.
4. Evaluate the Split Portions
Subdivision testing should represent the intended method, such as hand splitting or a defined mechanical device.
Depending on the product and regulatory strategy, レビュー:
- Ease of splitting.
- Fracture location.
- Segment mass variation.
- Material loss.
- Content uniformity.
- Friability of the resulting portions.
- Dissolution or release behavior.
- Stability of split portions where required.
Equal mass does not automatically prove equal active content. If the formulation contains an uneven distribution of active ingredient, two fragments with similar weight may still differ in drug content.
The FDA guidance is relevant to products intended for the United States. Worldwide projects must confirm requirements in each applicable market, particularly for modified-release products or dosage forms where subdivision may alter release behavior.
工具検査は製品の検証ではありません
The responsibility boundary should remain clear:
| 活動 | それが確認していること | 確認していないこと |
| 図面承認 | 意図された寸法と構成 | 完成したタブレット性能 |
| 工具検査 | 図面への適合性 | 信頼できる細分化 |
| 報道裁判 | 試験条件下での圧縮および取り扱いの挙動 | 完全な商業バッチ一貫性 |
| 医薬品検査 | 製品およびセグメントのパフォーマンス | あらゆるプレス条件下での長期金型寿命 |
A tooling supplier can manufacture and inspect a punch feature. The pharmaceutical manufacturer or product owner must validate the final tablet.
スコアリングタブレットツールを注文する前に準備すべき情報
A complete enquiry reduces the risk of designing the score without enough product or press information.
タブレットデータ
提供:
- タブレット形状.
- Diameter or major and minor dimensions.
- Overall thickness.
- カップ概要.
- Target number of portions.
- Required segment symmetry.
- Coating status.
- Logos, characters, or other face features.
- Intended hand or mechanical splitting method.
ブレークラインデータ
Define, where already established:
- Single- or double-sided configuration.
- 深さ.
- Width.
- 含まれる角度.
- 根半径.
- 長さ.
- Endpoint position.
- 向き.
- Relationship to logos or embossing.
Where the dimensions remain under development, identify them as proposed rather than validated.
処方およびプロセスデータ
Include relevant information such as:
- Development status of the formulation.
- Intended hardness range.
- Expected compression-force range.
- Known brittleness or elastic-recovery concerns.
- Ejection or take-off issues from prior trials.
- コーティング, パッケージング, and handling requirements.
A tooling supplier does not need the full confidential formulation to understand that the tablet’s fracture behavior and hardness range affect the score design. The level of disclosure can be agreed within the project.
プレスおよび工具データ
確認してください:
- Press model.
- Tooling standard.
- Punch type.
- Upper and lower punch nominal lengths.
- Keying requirements.
- Key orientation.
- Available lower-punch keying.
- Existing tooling drawings or samples.
- Inspection-document requirements.
SunshineProはカスタムサービスを提供しています タブレットプレス金型 from drawings or samples and lists size customization, material-selection support, CNC加工, 熱処理, and dimensional inspection. Final material, 幾何学, 検査範囲, and project suitability should still be confirmed for the specific enquiry.
最終設計審査原則
Before approving a scored-tablet tooling drawing, confirm five points:
- The score geometry has been reviewed relative to the tablet thickness, カップ概要, 定式化, and hardness range.
- The selected single- or double-sided configuration matches the intended fracture path.
- Opposed features have adequate alignment and upper/lower punch clearance.
- Compression, 射出, take-off, コーティング, パッケージング, and handling risks have been considered.
- The validation plan separates tooling conformance from whole- and split-tablet performance.
There is no universal break-line geometry that guarantees accurate splitting and long tool life. The most reliable approach is to combine a complete tablet specification, a controlled punch-face design, suitable press setup, and product-specific validation.
For a custom tooling enquiry, prepare the tablet drawing, score dimensions, プレス詳細, keying requirements, and requested inspection records before SunshineProへの連絡.



サンシャインより書かれました
サンシャインで, 私たちは精密金型部品の専門製造およびサプライヤーです, プレスおよび射出成形用途向けの幅広い製品を提供しています. 私たちの主な焦点はパンチダイスです, イジェクターピンとスリーブ, ガイドポストとブッシング. 高度なCNC加工技術で, 厳格な品質管理, そして強力な生産能力, 私たちは信頼性を保証しています, 高精度部品, また、迅速かつ効率的なグローバル供給のための在庫の標準部品も併用しています.
ニュース
サービスを受けましょう
あらゆる予算に合った高品質な部品と、親切なスタッフが訓練されていて、訪問を有益で手間なく充実させてくれます.
