



粘着やピッキングの問題に対するタブレットパンチコーティング
Tablet punch coatings can reduce some sticking and picking problems, but they are not a universal cure. Material may adhere to a punch because of formulation moisture, 潤滑不足, 熱, 報道条件, damaged tooling, unsuitable embossing, or the interaction between the formulation and punch surface. A coating should be selected only after these causes have been investigated.
Surface treatment is also only one part of the broader tooling decision. Different タブレットプレスの金型タイプ involve different punch geometries, 寸法, substrates, および運用要件. This guide focuses specifically on deciding whether a punch coating is appropriate, comparing common coating families, specifying the coated tool, and evaluating the result under production conditions.
パンチコーティングを選ぶ前に問題を特定しましょう
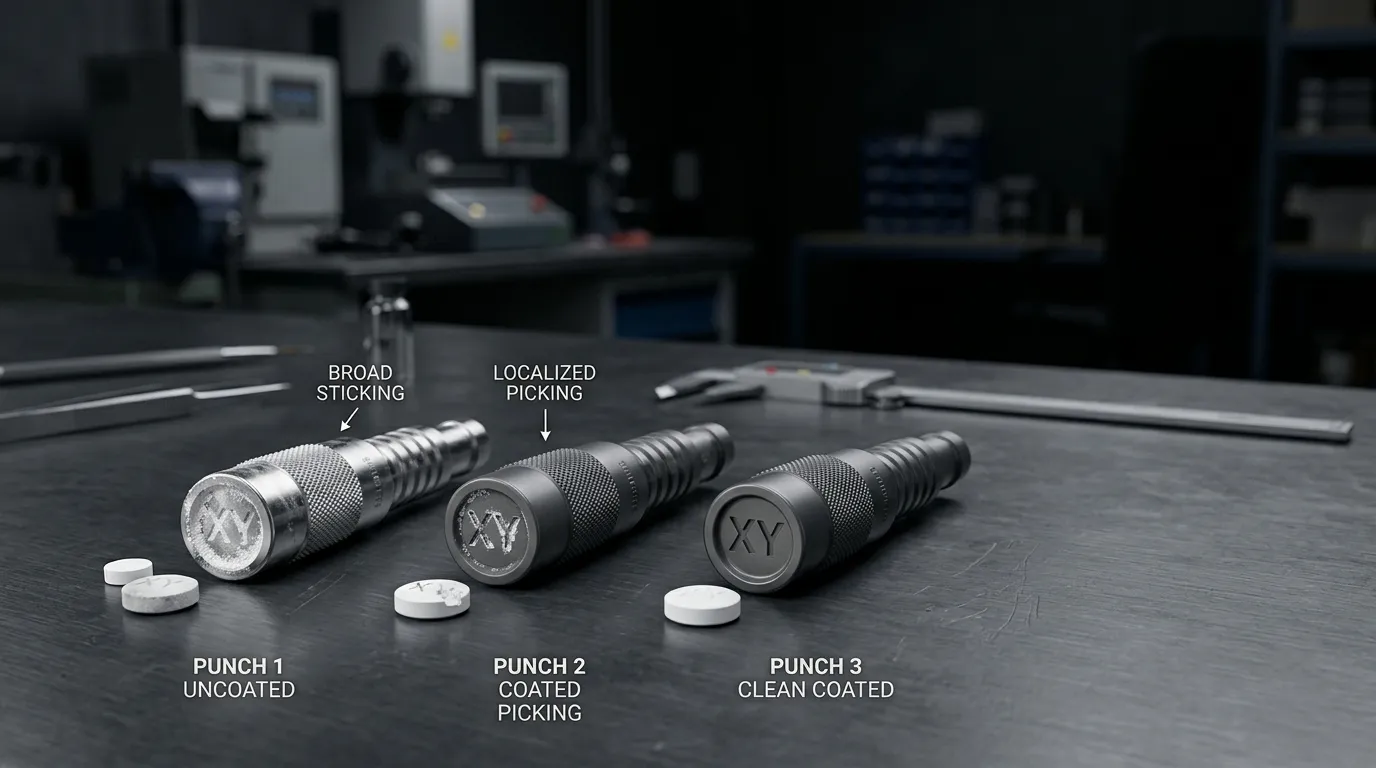
Sticking occurs when formulation material adheres to the punch face instead of remaining fully within the compressed tablet. The deposit may begin as a thin film and gradually become a visible layer that affects tablet appearance, weight consistency, 表面品質, or press operation.
Picking is more localized. Material is pulled from the tablet surface and collects inside or around recessed punch features such as letters, ロゴ, score lines, and small decorative details. A tablet may therefore show a damaged character or crater even when the rest of its surface appears acceptable.
The distinction matters because a coating selected for broad punch-face adhesion may not correct picking caused by sharp embossing corners, damaged lettering, or material trapped inside a narrow recess.
スティック, ピッキング, and Filming Are Not the Same Defect
| 症状 | 典型的な場所 | 最初の検査 | コーティングの関連性の可能性 |
|---|---|---|---|
| 撮影 | パンチフェイスの一部または全体に薄い層を塗っています | Check early buildup, 湿気, 潤滑, punch cleanliness, および表面状態 | 基本的な原因が制御された後、表面裁判を正当化する警告サインかもしれません |
| スティック | パンチカップや面の広い面積 | Review formulation properties, 熱, 圧力, 粗さ, 腐食, and run conditions | プロセス修正後も表面接着が持続する場合、コーティングが役立つことがあります |
| ピッキング | Embossing, ロゴ, score lines, or recessed details | Inspect character geometry, damaged edges, ポーランド語, and local material accumulation | Selective coating or a different surface system may help, but design changes may also be necessary |
The underlying mechanism involves competition between adhesion to the punch and cohesion within the compact. When formulation-to-tool adhesion becomes strong enough, material stays on the punch or is pulled from the tablet. ザ IQコンソーシアムによるタブレットの貼り付けとピッキングのレビュー describes the defect as a multifactorial problem involving API properties, 定式化, 金型, the tablet press, および処理条件.
次に塗るのが正しいかどうかを判断してください
A coating request should begin with a root-cause review. それ以外は, an expensive surface treatment may be used to compensate for a correctable formulation, equipment, or maintenance problem.
Check the following before comparing coating quotations:
- Inspect the punch surface. Look for scratches, corrosion pits, damaged polish, embedded residue, worn lettering, chipped edges, and local roughness. Surface defects can hold particles and create repeated buildup sites.
- Review moisture and hygroscopicity. A wet granulation, moisture-sensitive API, humid room, or condensation on cold tooling can increase adhesion. A coating cannot provide reliable control if the material condition changes significantly between batches.
- Review lubrication. 潤滑剤タイプ, amount, distribution, and blending can affect punch adhesion. Correcting lubrication requires formulation expertise because excessive or prolonged lubrication can create other tablet-quality problems.
- Check temperature and press conditions. Low-melting ingredients, extended compression, high operating speed, 摩擦, and heat accumulation can change the formulation’s behavior at the punch face.
- Examine cup and embossing geometry. Deep cups, narrow recesses, sharp character corners, and small lettering may concentrate material or make cleaning difficult.
- Compare when the defect begins. Immediate buildup may suggest a different mechanism from adhesion that develops only after a long production run.
- Confirm tooling cleanliness and handling. 汚染, improper storage, or unsuitable polishing can produce a surface that behaves differently from a new tool.
コーティング前に修正すべき条件
Coating should not be the first response when the main problem is:
- uncontrolled blend moisture or room humidity;
- 潤滑の不均一さ;
- residue from inadequate cleaning;
- visibly scratched, corroded, or damaged tooling;
- worn or unsuitable embossing;
- unstable press temperature or compression conditions;
- a formulation change that has not been evaluated;
- buildup caused by a specific mechanical defect.
These factors may remain active after coating and can shorten coating life or make a trial result difficult to interpret. Practical root-cause resources such as the タブレットの粘着とピッキングの14の原因 show why tooling surface treatment should be considered within a wider process investigation.
コーティングを評価する条件
A controlled coating trial becomes more reasonable when:
- sticking persists after moisture, 潤滑, 掃除, and press conditions have been stabilized;
- picking repeatedly occurs around fine embossed details;
- an abrasive formulation gradually damages the punch finish;
- corrosion creates pits that encourage further buildup;
- the current surface loses its finish too quickly during production;
- a documented formulation-to-surface interaction remains after other causes are addressed.
Even in these cases, coating should be treated as one part of the corrective plan rather than a guaranteed solution.
必要なコーティング機能を定義する
Buyers often begin by asking for a named coating. A better first question is: What must the surface do?
| 必要な機能 | 主な問題の解決 | 重要な選考点 |
| アンチスティック性能 | 配合の接着と蓄積 | Surface chemistry, フィニッシュ, 質感, 定式化の性質, coated area |
| 耐摩耗性 | 研磨による損傷とパンチディテールの喪失 | 硬度, コーティングの接着, substrate support, コーティング厚さ |
| 耐腐食性 | Chemical attack, staining, and pitting | Coating continuity, exposed edges, cleaning environment, formulation chemistry |
| 複合保護 | 接着と摩耗や腐食 | Trade-offs among finish, 耐久性, 次元制御, およびメンテナンス |
A very hard coating is not automatically the best anti-stick coating. Hardness mainly describes resistance to indentation or wear under a defined test method. Sticking also depends on surface chemistry, フィニッシュ, topography, 定式化の性質, 圧力, 温度, 潤滑.
A surface can be hard but still attract or mechanically trap a particular formulation. Conversely, a coating marketed for low adhesion may fail prematurely if it lacks sufficient wear resistance for an abrasive product.
Surface energy is another useful concept, but it should not be used as a single selection number. Research comparing differently coated punches found that formulation and coating interactions could not be predicted reliably from one surface property alone. The comparative イブプロフェンパンチコーティング研究 supports formulation-specific evaluation rather than a universal ranking.
一般的なタブレットパンチコーティングの比較
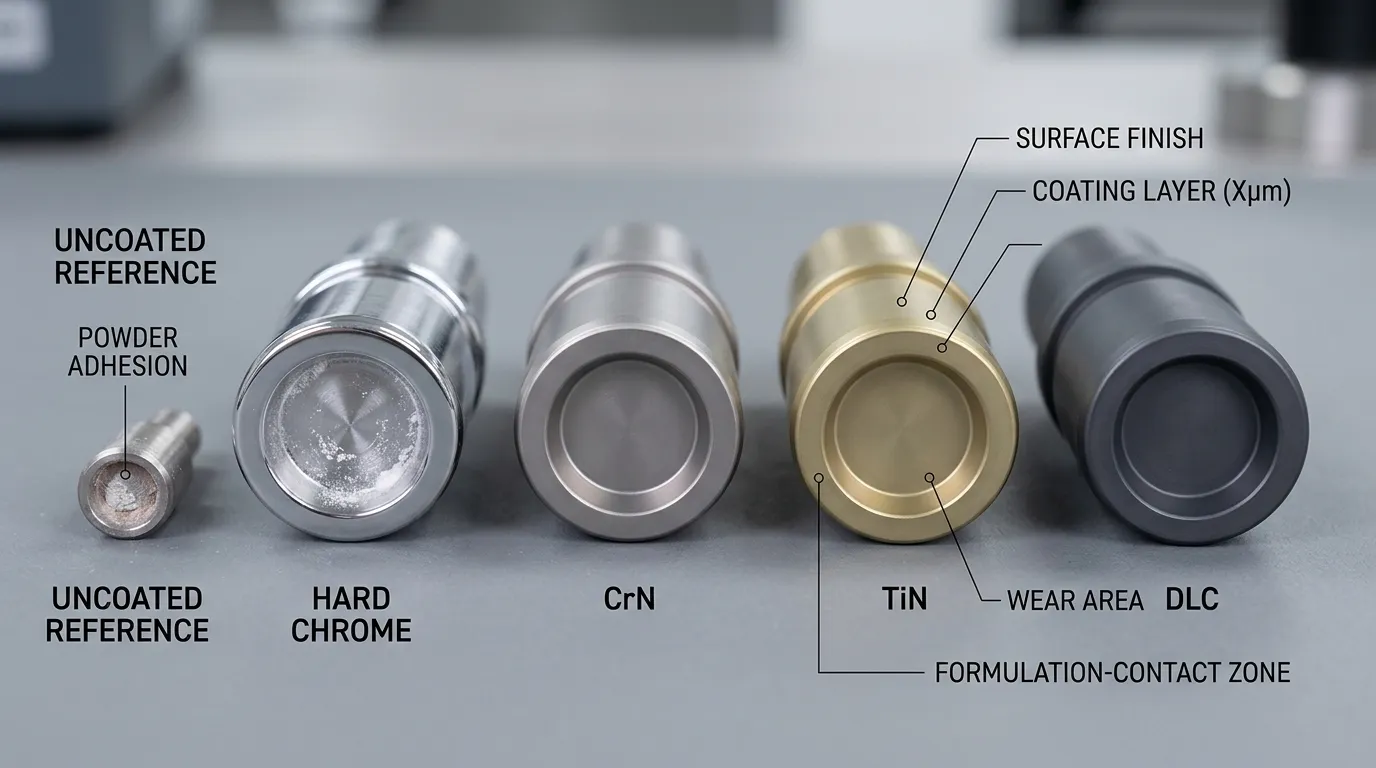
ハードクローム, chromium nitride, titanium nitride, ダイヤモンド様炭素, and proprietary textured systems frequently appear in tablet tooling discussions. Their names alone do not provide enough information for selection.
| コーティングファミリー | 一般的な位置 | 潜在的な利点 | 疑問と制限 |
| ハードクローム | Traditional plated surface for wear, フィニッシュ, and corrosion protection | Established process; can provide a hard, polishable surface | Thickness distribution, surface defects, edge buildup, post-polishing, and coating continuity must be controlled |
| クロム窒化物 | PVD coating often evaluated for adhesion, 使用期間, and corrosion requirements | 系に応じて複数の表面関数を組み合わせることができます | 標準的なCrNと独自の多層またはテクスチャ付きCrNは必ずしも同等ではありません |
| 窒化チタン | 耐磨性に一般的に関連する硬質PVDコーティング | 形状の保存や耐摩耗性が重要な場合に有用です | 高い硬度だけではアンチスティック適合性は証明できません |
| ダイヤモンド様炭素 | 炭素系コーティングシステムのファミリー | 摩耗や表面相互作用の有用な特性を提供する可能性があります | DLC composition, layer structure, deposition method, and substrate compatibility vary by supplier |
| 独自のテクスチャリングまたは多層システム | サプライヤーが開発したコーティング化学とエンジニアードサーフェスの組み合わせ | 特定の付着機構や製剤を標的にすることがあります | 製品固有の文書化と代表的な試験を用いて評価しなければなりません |
ハードクローム
Hard chromium is normally deposited by electroplating. It has a long history as a hard, corrosion-resistant surface treatment, but its performance depends on preparation, plating quality, thickness distribution, and final finishing.
For tablet punches, buyers should ask whether plating changes sharp edges, land areas, character details, or final dimensions. Surface pits, microdefects, and inconsistent coverage can become weak points or particle-retention sites. Polishing may improve the final finish, but it can also alter coating thickness or detailed features when poorly controlled.
Hard chrome should therefore be judged as a complete plated and finished system, not only by the word “chrome.”
クロム窒化物
Chromium nitride is commonly applied through physical vapor deposition, or PVD. It is frequently considered where sticking, 研磨摩耗, and corrosion resistance overlap.
CrN should not be treated as one standardized product. Different suppliers may use different pretreatments, layer structures, 厚さ, deposition conditions, and final finishes. Some proprietary systems also combine CrN chemistry with engineered surface texture.
This means performance data from one branded CrN system cannot automatically be transferred to another. The coating must be assessed with the actual formulation, punch design, 基質, および生産条件.
窒化チタン
Titanium nitride is widely recognized as a hard, wear-resistant PVD coating. It may be relevant when an abrasive formulation wears the punch face, lettering, or cup geometry.
Its hardness can make it attractive in comparison tables, but sticking is not purely a wear problem. A TiN-coated punch may still show adhesion if its surface chemistry, フィニッシュ, or formulation interaction is unsuitable.
TiN should be shortlisted when wear resistance is a primary objective, then tested for adhesion under the intended application rather than assumed to be an anti-stick solution.
ダイヤモンドライクカーボンおよび独自の表面システム
DLC refers to a family of carbon-based coatings rather than one uniform material. Suppliers may offer different compositions, layer structures, deposition methods, 厚さ, and surface finishes under the same broad category.
The same caution applies to proprietary multilayer or textured surfaces. A supplier may combine coating chemistry with a controlled topography designed for a particular sticking mechanism. That system should be evaluated according to its own documentation and trial data, not treated as identical to generic CrN, ティン, またはDLC.
専門記事 タブレットツールの性能向上のためのコーティングの選択 highlights the importance of coating adhesion, 基質の状態, 表面仕上げ, プロセス温度, 次元安定性, and uniformity. These engineering factors are often more useful than a simple list of coating trade names.
Match the Coating to the Formulation, 工具, and Application
Coating selection should reflect the actual failure environment.
A hygroscopic formulation may require better moisture control before any surface trial. A low-melting API may become more adhesive as compression and tooling temperatures rise. An abrasive mineral or nutraceutical formulation may require greater wear resistance to keep the punch surface smooth. A corrosive formulation may need a continuous protective barrier that prevents pits from developing.
Punch design changes the local conditions as well. Deep cups, detailed logos, narrow score lines, and small characters create different contact and release patterns from a simple flat-faced tool. Picking inside one letter may call for a different response from general filming across an entire punch cup.
Production conditions also matter. A coating that performs acceptably during a short, low-speed trial may behave differently during an extended run at commercial speed. The test should reproduce the pressure, 熱, cleaning cycle, and duration that contribute to the real problem.
なぜ基質の選択が表面処理よりも優先されるのか
The coating depends on the base tool for support. Tool steel, 熱処理, 硬度, 焼戻し条件, 清潔さ, 表面準備, and existing damage can all affect coating adhesion and durability.
A coating cannot restore a punch that is dimensionally unsuitable, heavily worn, ひび割れている, or improperly heat-treated. The coating process itself may also expose the tool to preparation or deposition conditions that must be compatible with the substrate.
詳細な成績選択は別のものに保管すべきです タブレット型材鋼選定 decision. For coating purposes, the essential questions are:
- What is the exact substrate?
- How was it heat-treated?
- What is its current surface and dimensional condition?
- Is the coating process compatible with that substrate?
- Will the final coating and finishing steps preserve the required geometry?
Specify the Coating, Coated Area, and Final Tool Requirements
A useful quotation request should define more than “anti-stick coating.” The buyer and supplier should agree on the functional and dimensional requirements of the finished punch.
Specify or request clarification on:
- the required function: anti-stick, 使用期間, 腐食, or combined protection;
- the coating family or proposed proprietary system;
- the deposition process;
- the exact coated area;
- whether coverage includes only the punch tip and cup or other tool regions;
- masking requirements;
- nominal coating thickness and allowable variation;
- surface finish before and after coating;
- treatment of embossing, score lines, 鋭い角, and edges;
- final punch dimensions after coating;
- coating adhesion or integrity inspection;
- substrate identification and heat-treatment condition;
- 掃除, 研磨, ハンドリング, and storage restrictions;
- wear-through and recoating criteria.
Selective coating can be useful when the problem is limited to the formulation-contact area. All-over coating may create different dimensional, ハンドリング, or cost considerations. The correct approach depends on the tool design and coating process.
Fine embossing deserves particular attention. Excessive buildup at an edge or inside a recess may reduce character clarity even when the rest of the coating is acceptable. The final inspection should therefore cover both overall dimensions and local detail.
SunshineProは次のように述べています。 タブレットプレス金型 can be custom processed from drawings or samples and that material inspection reports can be provided. 製品ページには高速鋼も掲載されています, CNC加工, 熱処理, custom sizes, and tablet punching-head customization. These verified tooling capabilities do not, by themselves, confirm the availability of any named coating or coating-deposition process.
コーティング業者と見積もりを評価しましょう
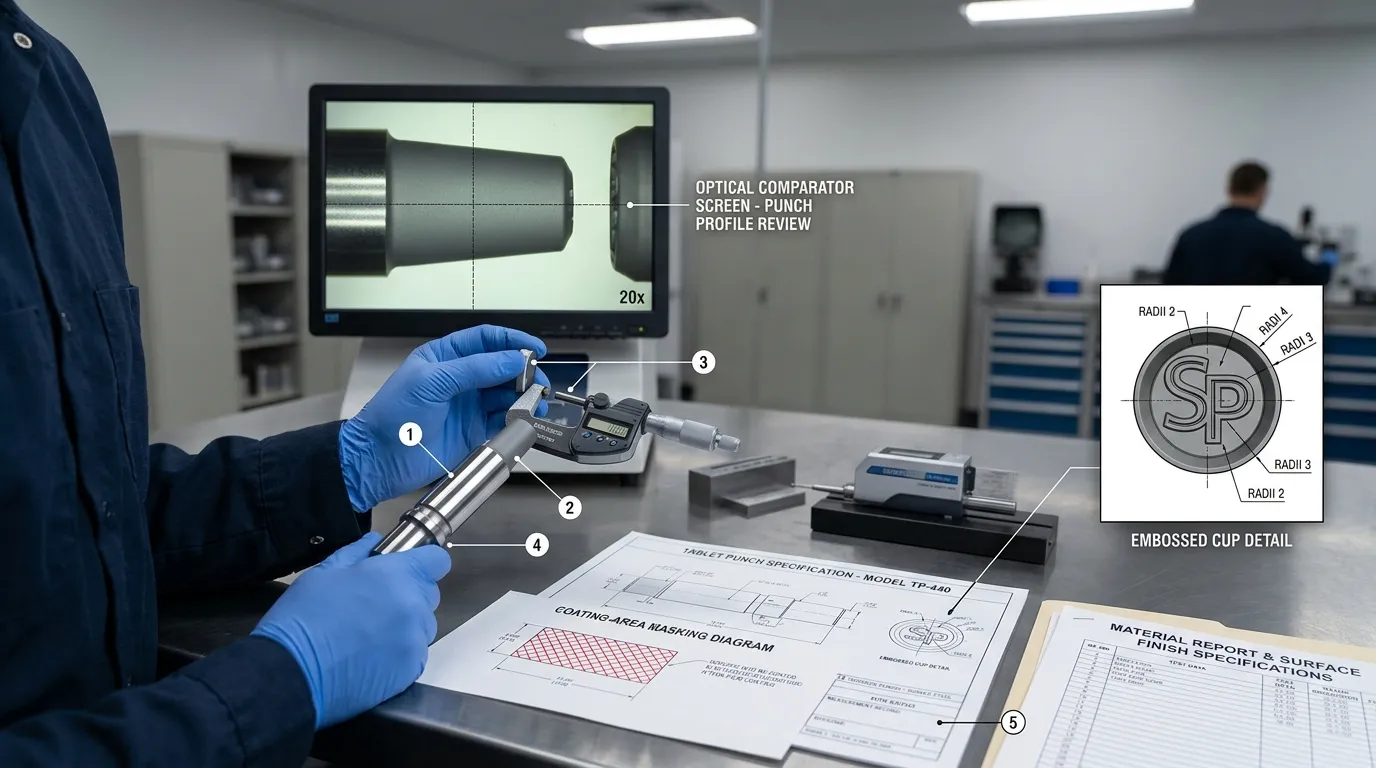
A strong supplier proposal should connect the recommended surface to the buyer’s formulation, 金型, failure pattern, および生産条件. A coating name and hardness claim are not enough.
RFQに含めるべき情報
Provide the supplier with:
- formulation type and known adhesion behavior;
- whether the problem is sticking, ピッキング, or filming;
- the exact location of buildup;
- how quickly the deposit develops;
- current punch material and heat-treatment information;
- photographs of the buildup and worn tooling;
- punch drawings, cup geometry, エンボス加工, and score details;
- tablet press model or applicable tooling standard;
- operating speed and relevant compression conditions;
- cleaning and polishing methods;
- current coating or uncoated baseline;
- known moisture, 温度, 使用期間, or corrosion concerns;
- the main objective: reduced adhesion, improved wear, corrosion protection, or a combination.
This information allows the supplier to evaluate the complete application instead of recommending a standard coating based only on the tablet shape.
サプライヤーからの要望書類と回答
サプライヤーに特定してもらう:
- the exact coating or proprietary system;
- the deposition process;
- compatible substrates and heat-treatment conditions;
- the areas that will be coated or masked;
- coating thickness and variation;
- expected final surface condition;
- how coating adhesion and integrity are inspected;
- how final punch dimensions and detailed features are checked;
- any prohibited cleaning or polishing method;
- how wear-through is identified;
- whether recoating is possible;
- what preparation is required for used tools;
- which material, プロセス, and inspection records are available.
Any performance figure should be accompanied by test conditions. A service-life claim based on one abrasive formulation, press, and cleaning routine may not apply to another application.
Regulatory suitability should also be reviewed using coating-specific documentation. General quality certifications or broad material statements do not prove that a surface is acceptable for every pharmaceutical product, API, market, or cleaning process.
代表的な生産条件下でのコーティングの検証
A coating should be compared under controlled conditions before it is adopted across a full tooling set.
- Establish a baseline. Record the performance of the current uncoated or existing coated tools.
- Define the acceptance criteria. Decide in advance what will be measured, such as buildup location, time before cleaning, tablet-surface quality, embossing clarity, tool wear, or coating damage.
- Control important variables. Keep the formulation, press, tooling geometry, 運用条件, and cleaning procedure as consistent as practical.
- Test under representative conditions. Use production-relevant speed, 圧縮, 熱, and run duration rather than relying only on a short laboratory test.
- Record the defect progression. Note when buildup begins, where it appears, and whether it stabilizes or worsens.
- Inspect the coating after the run. Look for scratches, wear-through, 欠け声, peeling, ひび割れ, 変色, and local loss around embossing.
- Compare the complete result. An apparent reduction in sticking should not be accepted if it introduces dimensional problems, damaged details, difficult cleaning, or coating-integrity concerns.
査読付き研究 工具コーティングを比較するための圧縮ツールボックス supports controlled comparison rather than assumptions based on coating labels. A trial with one formulation should also not be treated as proof that the coating will perform equally well with another API or process.
機能面を損傷せずにコーティングされたパンチを維持する
Coated punches may require different maintenance from uncoated tools. Cleaning or polishing methods that are safe for bare steel may scratch, 細い, or remove a functional coating.
Follow the coating supplier’s instructions and avoid assuming that one procedure applies to every surface. Maintenance should include inspection for:
- 局所的な摩耗;
- scratches or abrasion;
- チップス, ひび割れ, or peeling;
- corrosion near uncoated edges;
- loss of embossing clarity;
- increased cleaning frequency;
- renewed sticking in previously stable areas;
- damage caused by handling or storage.
The location of renewed buildup can help diagnose coating wear. If adhesion returns first around a letter edge or score line, the local surface may have worn or been damaged even when the wider punch face still looks acceptable.
Recoating is not always the correct response. The supplier should inspect the substrate, remaining dimensions, 表面損傷, and detailed geometry before deciding whether stripping and recoating are technically suitable. Worn or damaged tools may need replacement instead.
コーティングの選択は完全な工具決定の一部として活用しましょう
A defensible coating decision follows a clear sequence:
- identify whether the defect is sticking, ピッキング, or filming;
- correct formulation, 掃除, プロセス, and damaged-tooling causes;
- define whether anti-stick, 使用期間, 腐食, or combined protection is required;
- match the coating system to the formulation, 基質, 幾何学, および生産条件;
- specify the coated area, 表面仕上げ, 寸法, and required documentation;
- compare supplier proposals using the same criteria;
- validate the selected surface against an established baseline;
- maintain and inspect the coated tools according to supplier instructions.
SunshinePro’s website confirms custom tablet punches and dies made from drawings or samples, with high-speed steel, CNC加工, 熱処理, カスタマイズ, and material inspection reports listed on its tablet tooling page. It does not currently verify a named tablet punch coating portfolio, so coating availability and technical details should be confirmed for the specific inquiry.
To discuss the base tooling, ドローイング, 寸法, 材料要件, and operating context, 工具要件をSunshineProに提出してください. Include the sticking or picking pattern and the coating questions from this guide so the technical review can begin with the actual application rather than a generic coating request.



サンシャインより書かれました
サンシャインで, 私たちは精密金型部品の専門製造およびサプライヤーです, プレスおよび射出成形用途向けの幅広い製品を提供しています. 私たちの主な焦点はパンチダイスです, イジェクターピンとスリーブ, ガイドポストとブッシング. 高度なCNC加工技術で, 厳格な品質管理, そして強力な生産能力, 私たちは信頼性を保証しています, 高精度部品, また、迅速かつ効率的なグローバル供給のための在庫の標準部品も併用しています.
ニュース
サービスを受けましょう
あらゆる予算に合った高品質な部品と、親切なスタッフが訓練されていて、訪問を有益で手間なく充実させてくれます.
